The 2026 market for A3 / A4 TPU UV DTF Film Sheets is becoming more practical, not simply larger. Grand View Research identifies UV printing as a growing digital-printing segment, while Smithers continues to report strong demand for short-run, customized graphics. These trends matter to global buyers. They signal more orders for compact equipment, faster decoration, and films that perform across glass, metal, plastic, leather, and coated surfaces.
Quality still depends on details that product pages often hide. A reliable TPU film should offer stable dimensional behavior, clean adhesive transfer, suitable elasticity, and consistent curing under UV exposure. Check liner release with a small test. Watch the printed edge under angled light. Poor bonding may appear only after washing, bending, or temperature changes. FESPA’s technical guidance repeatedly stresses application testing, substrate preparation, and process control. That advice is easy to ignore. It should not be.
Marco Boer, Vice President of IT Strategies, has often expressed a useful digital-printing principle: “Digital printing is a business strategy, not merely a technology.” His point fits this category well. A3 / A4 TPU UV DTF Film Sheets are not judged by size alone. Buyers must compare adhesion, finish, handling, storage life, and total waste. This guide evaluates those practical factors for distributors, print shops, and brand owners. It will not pretend that one film suits every climate or substrate. Humidity changes everything. Supplier claims also deserve verification. Small tests remain wiser than expensive assumptions.
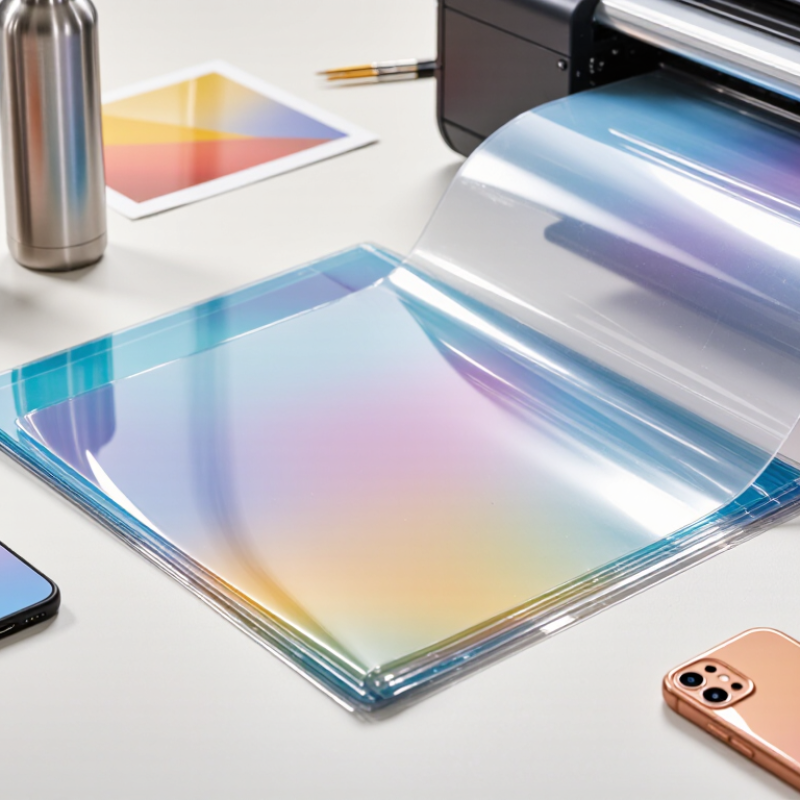
A3 and A4 formats suit different production rhythms. A3 measures 297×420 mm, while A4 measures 210×297 mm. A3 holds larger graphics, paired logos, and sleeve artwork with fewer joins. A4 works well for samples, small labels, and short custom orders. During testing, I find A4 easier to align on compact worktables. However, A3 reduces film waste when several small designs share one sheet.
Market data supports this shift toward digital decoration. Fortune Business Insights values the global digital printing market at about USD 35.71 billion in 2024. Its forecast reaches USD 58.56 billion by 2032. This does not measure TPU UV DTF alone. It shows stronger demand for flexible, short-run production. Grand View Research also forecasts double-digit growth for UV printing through 2030. Buyers should still check adhesion, curing consistency, and storage stability. A larger sheet cannot fix poor surface preparation.
Tips: Keep A3 and A4 sheets flat, dry, and dust-free. Leave a small margin around detailed artwork. Test white ink density before production. A4 is safer for trials, but A3 may improve batch efficiency. I sometimes prefer A4 for complex designs, although that choice can increase handling time. Ask for batch data, not only attractive samples.
TPU UV DTF film sheets use four functional layers: PET carrier, release layer, ink, and adhesive. The PET carrier provides flatness during printing and handling. It should resist curling in warm workshops. The release layer controls how easily the printed image leaves the carrier. If release is too weak, transfer becomes slow. If it is too strong, edges may lift or details may tear. The ink layer usually contains color, white ink, and protective varnish. These layers create sharp graphics on smooth, curved, or lightly textured surfaces. The adhesive layer then supports bonding after transfer pressure is applied.
A3 sheets suit medium designs, while A4 sheets help reduce waste for small logos and samples. In practical testing, I check fine lettering, edge adhesion, and surface clarity after 24 hours. Results can change with pressure, temperature, and substrate cleanliness. This is where specifications alone may mislead. A film that performs well on glass may behave differently on coated plastic. TPU also offers useful flexibility, but excessive stretching can distort narrow lines.
Tips: Store sheets flat in a dry, dust-free area. Keep the protective packaging closed. Test one sheet before production. Inspect release, color density, and adhesive coverage under normal lighting. Humidity deserves attention. It is often overlooked. Different regions may require different storage controls.
2026 Best A3 A4 TPU UV DTF Film Sheets for Global Buyers
UV DTF curing commonly uses 395–405 nm ultraviolet exposure. The correct wavelength alone does not guarantee strong adhesion. Lamp intensity, exposure time, distance, ink thickness, and film coating all affect the result. A3 and A4 TPU sheets should receive even exposure across the full printed area. Dark graphics and heavy white ink layers may need additional curing. Over-curing can make the adhesive layer brittle.
In practical testing, I place the film flat and keep the lamp distance consistent. I check the surface for tackiness, edge lifting, and visible ink softness. It should feel dry, not rubbery. Clean glass, coated metal, plastic, and ceramic surfaces differently, so one setting rarely fits every application. Humidity and dust also reduce bonding reliability. Small details matter.
A useful process includes a short exposure trial, a controlled transfer, and a peel check after 24 hours. I have seen attractive prints fail because the receiving surface was oily. That mistake is easy to repeat. Cross-hatch testing can reveal weak adhesion, but excessive pressure may distort soft TPU. Record lamp power, distance, exposure time, and room conditions for each batch. Some sheets behave differently between production lots, so verification remains necessary.
2026 Best A3 A4 TPU UV DTF Film Sheets for Global Buyers
Film selection should begin with thickness, not price. In production trials, thinner TPU sheets often conform better to curved surfaces. However, they may wrinkle during lamination or manual transfer. Thicker films provide stronger handling and improved dimensional stability. They can feel less flexible on narrow edges. For A3 and A4 formats, check whether the sheet remains flat after storage. A curled corner can disturb alignment and waste printed material.
Flexibility must match the object’s shape and use. Test a finished transfer around a bottle, case, or textured panel. Bend it repeatedly, then inspect the edges under bright light. Surface energy also matters. A film with suitable surface energy accepts ink evenly and reduces pinholes, weak bonding, and uneven gloss. Operators should test actual ink, adhesive, and substrate combinations. Laboratory values alone can mislead.
Durability testing should include rubbing, moisture exposure, and temperature changes. A practical trial uses printed samples from the same batch, not only a supplier’s demonstration piece. Compare adhesion after 24 and 72 hours. Keep records of temperature, pressure, and curing time. Small differences matter. No specification sheet tells the whole story. I have seen a flexible film fail because the adhesive layer was poorly matched. That result deserves review, not a quick rejection. Global buyers should request samples, technical data, and consistent batch controls before choosing A3 or A4 TPU UV DTF sheets.
For 2026 purchasing, global buyers should compare A3 and A4 TPU UV DTF film sheets by actual performance, not only price. Confirm sheet dimensions, cutting accuracy, and edge quality. A practical tolerance is often stated in millimeters, but suppliers may calculate it differently. Request a measured sample report. Do not assume the listed size is the usable area.
Roll width matters when sheets are converted, packed, or used with existing equipment. Check whether the width includes edge waste. For regular orders, compare the supplier’s minimum order quantity with your storage capacity and testing budget. A low MOQ can reduce risk, while a large MOQ may improve unit cost. Both can be misleading. Ask about film thickness, adhesive behavior, curing conditions, release stability, and storage temperature. Test several batches, because one successful sample proves little.
Tips: Measure twice. Record humidity. Keep samples sealed. Compare A3 and A4 sheets under the same application settings. Request technical data, safety information, material composition, and traceability documents before purchase. Compliance requirements vary by destination, so buyers should verify labeling, packaging, chemical restrictions, and import documentation with qualified local advisers. Supplier claims deserve evidence. I have found that missing documents often create more delay than poor pricing. A checklist helps, but it should be revised after every shipment.
„Thanks to the LUVIR technology, the solder resist process could be switched directly from the previously used mask exposure to direct exposure. As an outstanding digital solution on the market, this technology has been able to demonstrate fast process times and superior quality on our certified conventional ink in production. This allowed us to fully digitize the solder mask process at low cost – without process or ink adjustments. An excellent benefit to our production in Rot am See.“
Ralf Göhringer (Head of Production WE Rot am See)
I would definitely recommend the Limata machine and team for a future company purchase
Michael Greenaway
Compunetics Inc.
“The Limata ldi has been amazing!! Best thing we did was buy this machine”
Richard Brady
GM
Circuitlabs
“Since 2019, we have been running the Limata X1000 LDI system (including LUVIR for solder mask imaging) in daily production as an addition to our current process with film. The machine was capable of properly exposing Taiyo PSR-4000 BN (DI) solder mask types on normal to high-copper boards using a new and unique direct imaging process. The machine operating interface is very user friendly which allowed for a quick technical training curve. The pre-registration processing reduced several seconds of production time at every print. Limata support and service staff is incomparable. They supported our team every step of the way at basically any time of the day or night, with literally, an immediate response time, customizing the software interface to best fit our Operations and needs.
We have exposed more than 8,000 prints since end of October, on various solder mask colors and some resist film panels. Limata, has proven to be very capable and innovative. They are a strong contender in the industry.
We have very much enjoyed this project, and working with the team!
Thank you Limata for the continued support and being a part of our growth.”
Bill Sezate
Vice President, GM
Summit Interconnect
As a replacement to our current contact exposure process with film, the LIMATA X2000 system including LUVIR-Technology was capable of properly exposing non-LDI solder mask types using a direct imaging process. The machine offers cutting edge software with a very intuitive operating interface which allowed for quick technician training curve. The dual drawer system combined with pre-registration processing reduced several seconds of production time at every machine cycle. Limata support and service staff is world class. They added software patches to keep production running at shortest possible response times, customized the software interface to best fit our in-house Operations system, and even wrote a step-by-step machine processing manual. As a result of the project, we have exposed more than 16,000 times on various product types and solder mask brands/colors. Limata, in a very short timeframe as a company, has definitely shown they are truly innovative and will be challenging the industry of direct imaging for the top spot.
Kevin Beattie
Process Engineer
TTM Technologies
Forest Grove Division