In 2026, Power Factor Correction Ckd solutions deserve careful evaluation, not a one-size-fits-all promise. Poor power factor can increase current for the same useful power, adding stress to cables, transformers, and switchgear. The U.S. Department of Energy’s Improving Motor and Drive System Performance sourcebook reports that motor-driven systems account for about 54% of U.S. manufacturing electricity use. That figure makes industrial power quality a practical concern, though it does not mean every facility needs the same correction design.
The details matter. A CKD package may simplify shipping and on-site assembly, but its capacitors, switching equipment, protection, and controller must match the actual load. IEEE Standard 1459 provides accepted definitions for power quantities used in measurement and analysis. Power-quality researcher Alexander E. Emanuel’s published work emphasizes the importance of defining those quantities consistently before assessing system performance. This is a paraphrase of his technical work, not a verified verbatim quotation.
A reliable comparison starts with measured load profiles, harmonic conditions, operating hours, and utility billing rules. A capacitor bank sized from a single snapshot may underperform when production changes. Small details matter. This guide examines how to compare 2026 Power Factor Correction Ckd options, what data to request, and which installation questions can prevent avoidable costs. Results vary by site. Buyers should verify manufacturer specifications and have qualified engineers review system measurements before selecting equipment.
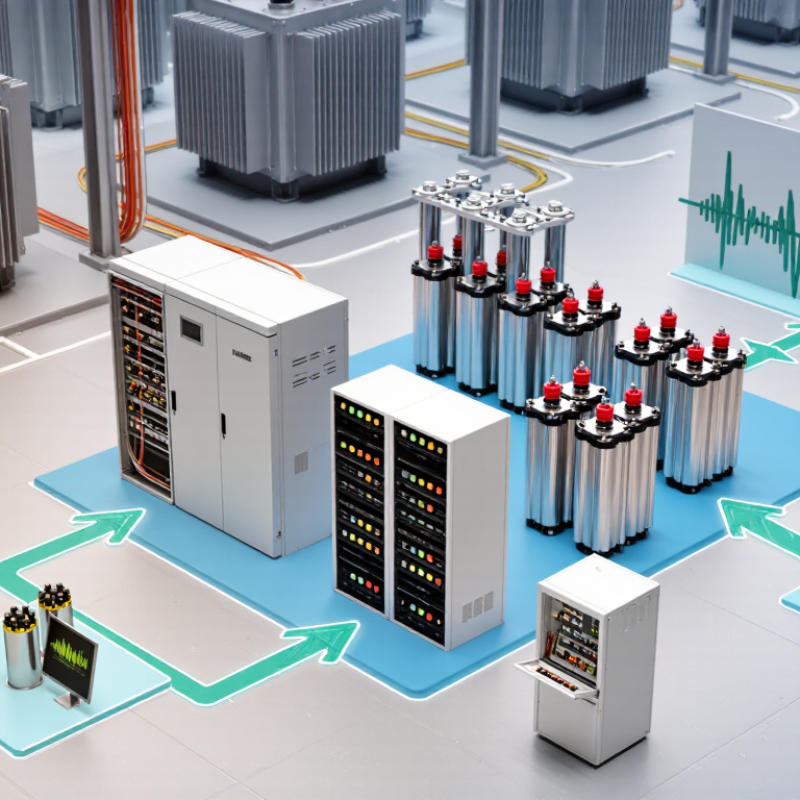
Power factor correction reduces the reactive power drawn by many electrical loads. Motors, pumps, and older fluorescent lighting can all contribute to a low power factor. In a CKD system, equipment is supplied in components for assembly near its installation site. That approach can simplify transport, but it does not remove the need for careful electrical design.
A correction system often uses capacitor banks switched in stages as demand changes. Harmonic measurements matter: drives and other non-linear loads can interact with capacitors and cause overheating or unwanted resonance. A site assessment should review load profiles, existing protection, and available panel space. Small details count. Cable lengths and ventilation affect how reliably assembled equipment performs.
CKD planning also depends on clear drawings, labeled parts, and assembly checks. Commissioning should confirm connections, protection settings, and power factor under representative operating loads. I would not call this plug-and-play. Local conditions may differ from the design assumptions, and real loads rarely stay perfectly steady. An experienced electrical engineer can verify the solution against measured site data and applicable requirements.
A CKD power factor correction solution helps an electrical system use power more efficiently. Motors, pumps, and compressors draw reactive power, which makes current lag behind voltage. Capacitors provide reactive power locally, reducing the amount the supply must deliver. The principle is simple. Lower reactive demand can reduce current in cables and transformers, though actual savings depend on the installation.
A controller monitors the power factor through current transformers and voltage signals. When the reading falls below a set target, it switches capacitor stages on. As loads change, it adds or removes stages to avoid overcorrection. You may hear contactors click inside a panel during this process. That matters. A well-sized system responds to real operating conditions rather than correcting for a single snapshot.
CKD configurations can be assembled to suit site requirements, but component selection needs care. Engineers should check load patterns, capacitor ratings, switching frequency, and harmonic distortion before choosing a design. Harmonics can overheat capacitors, so filters may be needed in some facilities. A tidy calculation can still miss a rarely used machine or a sharp load change. Regular inspections help reveal hot connections, worn switching parts, and falling capacitance.
A CKD power factor correction system arrives as separate components for assembly and integration. Its core is the capacitor bank, which supplies reactive power close to the electrical load. Capacitors are grouped in steps so the system can respond to changing demand. Small steps offer finer adjustment, but add switching complexity.
The controller measures power factor through a current transformer and switches capacitor steps as needed. Contactors suit many standard applications; thyristor switches can respond faster when loads change rapidly.
Fuses or circuit breakers protect each step, while discharge resistors reduce residual voltage after disconnection. Safety matters. A detuned reactor may be added where harmonics are present, but its rating should follow measured site conditions. Guessing can create trouble.
Busbars, terminals, and the enclosure complete the assembly. Clear wiring diagrams and labeled connections help technicians check each stage during commissioning. Ventilation also matters: heat can shorten capacitor life, especially in a crowded cabinet.
CKD assembly allows local adaptation, though it places more responsibility on the integrator. That part is easy to underestimate. Verify voltage, current, temperature, and harmonic levels under real operating conditions; readings taken during a quiet shift may not tell the whole story.
Evaluating CKD solutions for 2026 applications starts with the load, not the catalogue. Record real and reactive power across a typical operating cycle, including quiet shifts and motor starts. A single reading can hide large changes. Check whether loads use variable-speed drives, welders, or other equipment that may produce harmonics.
For a CKD package assembled on site, confirm that components, wiring diagrams, protection devices, and assembly instructions match the proposed design. Ask how capacitor stages switch as demand changes, and whether the system could overcorrect during light-load periods. If harmonic levels are significant, a qualified engineer should assess whether detuned reactors or other measures are appropriate. Measure under load.
Compare the rated voltage, temperature limits, enclosure, and maintenance access with the actual installation environment. Dust near a production line or heat inside a crowded electrical room can shorten component life. Request test records and clear commissioning procedures, not just a power-factor target. That matters. Also check whether replacement parts and technical support will be available locally. A CKD design may lower shipping or assembly costs, but local integration can introduce errors; terminal torque and protection settings deserve careful verification. No spreadsheet can replace a site inspection.
For a CKD power-factor-correction package, treat installation as an engineering task, not just a panel assembly. Confirm the site voltage, load profile, available fault current, and harmonic levels before sizing capacitor steps. The U.S. Department of Energy’s 2014 motor-systems sourcebook estimates that motor-driven systems use about 68% of U.S. manufacturing electricity. That makes changing motor loads a practical concern: a bank sized for one shift may overcorrect during lighter operation. Install current transformers in the correct orientation, provide ventilation, and keep capacitors away from heat sources. Small details matter.
Commission the system under representative operating conditions. Record power factor, current, voltage, and capacitor-step status at different load levels, then compare readings with the utility meter. IEEE 519-2022 sets voltage total harmonic distortion limits of 8% at 1 kV and below, and 5% from 1 kV to 69 kV. These are assessment limits, not a substitute for checking the equipment manufacturer’s ratings. If harmonics are elevated, have a qualified engineer assess resonance risk before adding capacitors or detuned reactors.
Monitoring should flag repeated switching, rising capacitor temperature, blown fuses, and declining capacitance. During planned maintenance, isolate the bank, verify discharge, and inspect terminals for looseness or discoloration. Keep a dated record of measurements; otherwise, a slow decline can look normal. I would not assume a clean commissioning report means the job is finished. Load patterns change, and maintenance intervals may need adjustment.
„Thanks to the LUVIR technology, the solder resist process could be switched directly from the previously used mask exposure to direct exposure. As an outstanding digital solution on the market, this technology has been able to demonstrate fast process times and superior quality on our certified conventional ink in production. This allowed us to fully digitize the solder mask process at low cost – without process or ink adjustments. An excellent benefit to our production in Rot am See.“
Ralf Göhringer (Head of Production WE Rot am See)
I would definitely recommend the Limata machine and team for a future company purchase
Michael Greenaway
Compunetics Inc.
“The Limata ldi has been amazing!! Best thing we did was buy this machine”
Richard Brady
GM
Circuitlabs
“Since 2019, we have been running the Limata X1000 LDI system (including LUVIR for solder mask imaging) in daily production as an addition to our current process with film. The machine was capable of properly exposing Taiyo PSR-4000 BN (DI) solder mask types on normal to high-copper boards using a new and unique direct imaging process. The machine operating interface is very user friendly which allowed for a quick technical training curve. The pre-registration processing reduced several seconds of production time at every print. Limata support and service staff is incomparable. They supported our team every step of the way at basically any time of the day or night, with literally, an immediate response time, customizing the software interface to best fit our Operations and needs.
We have exposed more than 8,000 prints since end of October, on various solder mask colors and some resist film panels. Limata, has proven to be very capable and innovative. They are a strong contender in the industry.
We have very much enjoyed this project, and working with the team!
Thank you Limata for the continued support and being a part of our growth.”
Bill Sezate
Vice President, GM
Summit Interconnect
As a replacement to our current contact exposure process with film, the LIMATA X2000 system including LUVIR-Technology was capable of properly exposing non-LDI solder mask types using a direct imaging process. The machine offers cutting edge software with a very intuitive operating interface which allowed for quick technician training curve. The dual drawer system combined with pre-registration processing reduced several seconds of production time at every machine cycle. Limata support and service staff is world class. They added software patches to keep production running at shortest possible response times, customized the software interface to best fit our in-house Operations system, and even wrote a step-by-step machine processing manual. As a result of the project, we have exposed more than 16,000 times on various product types and solder mask brands/colors. Limata, in a very short timeframe as a company, has definitely shown they are truly innovative and will be challenging the industry of direct imaging for the top spot.
Kevin Beattie
Process Engineer
TTM Technologies
Forest Grove Division
