The 2026 Top Organic Fertilizer Processing Plant Suppliers market reflects a larger shift toward soil restoration, resource efficiency, and traceable production. FiBL and IFOAM Organics International reported 96.4 million hectares of organic farmland worldwide in 2022. Their latest statistics also valued the global organic food market at approximately €134.8 billion. These figures do not prove every fertilizer supplier performs equally well. They show why dependable processing equipment matters.
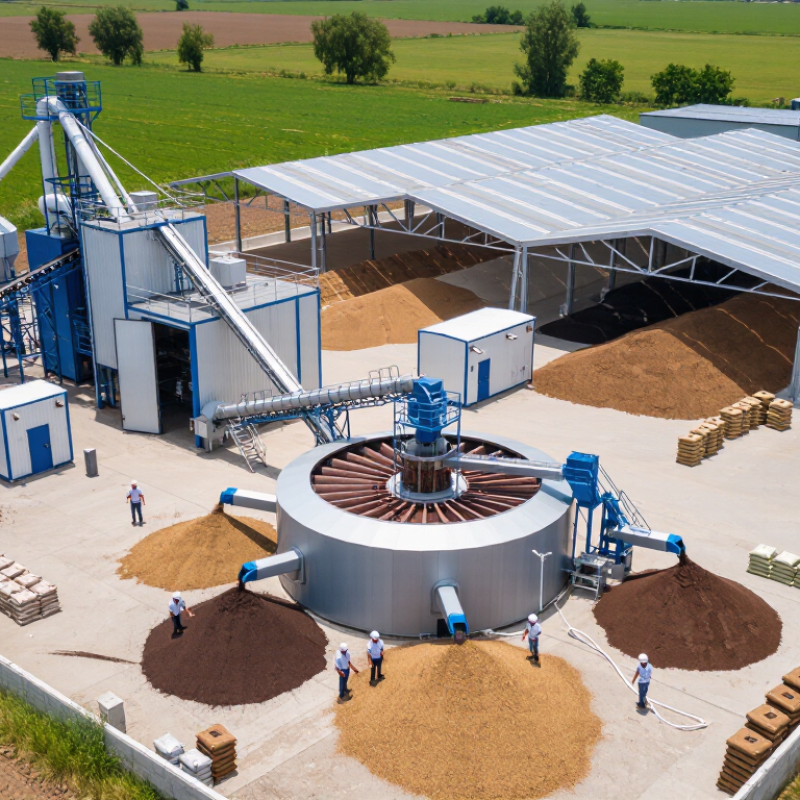
A capable Organic Fertilizer Processing Plant should handle manure, crop residues, compost, and other approved organic inputs safely. Practical evaluation begins with moisture control, odor management, compost maturity, and contamination screening. A rotary drum granulator may improve product consistency, while a curing area helps stabilize nutrients before packaging. Operators should also inspect dust collection systems, temperature records, laboratory testing, and after-sales service. Small details matter. Wet granules can collapse inside the dryer.
Ronald Vargas, a soil scientist associated with the Food and Agriculture Organization, has stated, “Soils are the basis of life on Earth.” His point remains highly relevant for fertilizer manufacturers. The United Nations Food and Agriculture Organization continues to emphasize soil health, nutrient cycling, and sustainable land management in its technical reports. Suppliers should therefore offer more than impressive capacity figures. They need documented performance, transparent specifications, and practical installation experience.
This guide compares leading suppliers through a cautious lens. Energy use, raw-material flexibility, maintenance access, and product quality receive close attention. Some market claims remain difficult to verify. That weakness deserves honest discussion, especially when buyers invest in a complete processing line.
2026 Top Organic Fertilizer Processing Plant Suppliers
Organic fertilizer plants begin with clean, traceable feedstocks. Common inputs include livestock manure, crop residues, food scraps, and green waste. The World Bank’s What a Waste 2.0 report estimates that organic materials represent about 44% of global municipal solid waste. This creates opportunity, but contamination remains a serious risk. Plastics, treated wood, and chemical residues can reduce product safety and processing value.
Biology controls the core conversion stage. Aerobic composting needs oxygen, moisture, and balanced carbon and nitrogen. Many technical guidelines target a carbon-to-nitrogen ratio near 25–30:1. The active pile often reaches 55–70°C when mixing and airflow work properly. Excess heat can damage beneficial organisms. Low heat may indicate poor aeration or an unsuitable feedstock mix. After biological treatment, plants commonly use screening, crushing, granulation, drying, cooling, and final quality testing. FiBL’s 2024 report recorded 96.4 million hectares under organic agriculture globally in 2022. That expanding production base increases demand for reliable soil inputs, but not every plant design fits every region.
Tips: Ask suppliers for a mass-balance calculation, laboratory test results, odor-control plans, and maintenance records. Verify moisture, nutrient content, pathogens, heavy metals, and maturity before purchase. A shiny granulator is not enough. Feedstock consistency matters more than brochure capacity. Real facilities also need drainage, dust control, trained operators, and flexible recipes. Some designs look efficient on paper, yet fail during rainy seasons or feedstock shortages. That weakness deserves honest review.
Reliable composting begins with measurable process control, not attractive equipment. In pilot batches, operators should maintain temperatures at or above 55°C for several consecutive days. This benchmark supports safer, more stable organic fertilizer production. However, temperature alone can mislead. A dry center may show uneven heating, while a wet pile may lose oxygen quickly.
Moisture commonly performs best around 50–60%. A handful should feel damp, not drip. Aeration needs regular turning, airflow channels, or controlled ventilation. Oxygen-starved material develops sour odors and dark, sticky pockets. Processing plant teams should record temperature, moisture, turning times, and feedstock changes. These records improve traceability and help suppliers adjust equipment settings. Our early trials relied too heavily on temperature readings. That was a mistake. Moisture distribution mattered more than expected.
Tips: Use multiple temperature probes at different depths. Turn the pile when heat drops or odors increase. After active composting, allow at least two to four weeks of curing, depending on feedstock and climate. Mature compost should smell earthy, feel crumbly, and show no obvious heating after mixing. A simple seed-germination check can reveal remaining instability. Do not rush curing. Even well-heated material may still contain phytotoxic compounds.
A serious supplier screen starts with N-P₂O₅-K₂O, not brochure claims. Require laboratory results on a dry-matter basis, batch frequency, and sampling methods. The FAO Fertilizer and Plant Nutrition reports emphasize balanced nutrient management, but organic inputs vary sharply by feedstock. A compost plant may show 2-2-2, while poultry-based material can exceed 3% nitrogen. Those figures need verification.
Throughput must match actual moisture conditions. Ask for tonnes per hour at 55%, 65%, and 75% moisture, not only rated capacity. The European Commission’s Joint Research Centre links biological waste treatment performance with aeration, moisture, and residence time. Its waste-treatment reference data indicate electricity use can range roughly from 10 to 40 kWh per tonne. Screens, mixers, dryers, and pelletizers may push consumption higher.
Energy claims deserve skepticism. Real production rarely matches laboratory efficiency. Request monthly kWh records, feedstock moisture, downtime, and finished-product output. Compare energy per saleable tonne, not per incoming tonne. A 2024 International Energy Agency efficiency framework also supports measuring energy intensity against operating conditions. This screening method is imperfect. I would still reject any supplier hiding nitrogen losses, unstable throughput, or unexplained energy figures. Test certificates should come from competent laboratories, with traceable methods and recent sampling dates.
2026 Top Organic Fertilizer Processing Plant Suppliers should be evaluated by production category, not by price alone. Compost lines handle aerobic decomposition, turning, screening, and controlled moisture. Vermicompost lines need gentler feeding systems, shaded beds, and stable temperature control. These details affect nutrient quality and worm survival.
Pellet lines compress prepared organic material into dense, easy-to-transport fertilizer. Granule lines often use disc or drum granulation, followed by drying, cooling, and screening. A suitable supplier should explain capacity, moisture range, power demand, spare parts, and cleaning procedures. Ask for test results using your own raw materials. A glossy quotation proves little. I have seen efficient equipment perform poorly when feedstock changes from manure to crop residue. That risk deserves honest discussion.
Tips: Check the full process flow, not one machine. Request a small material trial before signing. Measure output size, dust, moisture, and energy use. Leave room for maintenance access. No line is perfect. A strong supplier admits its limits and suggests practical adjustments. Also inspect operator training, warranty terms, installation support, and safety controls. These factors often decide whether a compost, vermicompost, pellet, or granule plant performs reliably after commissioning.
Indicative commercial processing-line throughput ranges by product category
Compost and vermicompost lines generally operate at lower throughput because biological processing requires longer residence times. Pellet and granule lines can achieve higher mechanical output after drying and conditioning. The ranges represent commonly published equipment specifications and are not a supplier ranking; actual capacity depends on feedstock, moisture, formulation, and configuration.
Compliance Standards: EU 2019/1009, USDA NOP, and ISO 14001
Reliable organic fertilizer suppliers should treat compliance as a working system, not a marketing phrase. Under EU 2019/1009, producers may need evidence for product categories, safety limits, labeling, traceability, and conformity assessment. Batch records should connect raw materials to finished granules, bags, and delivery documents. Moisture, nutrient content, pathogens, and contaminants also require controlled testing. Small documentation gaps can delay market access.
USDA NOP requirements focus on approved inputs used in organic production and handling. Suppliers should maintain current ingredient information, process descriptions, and supporting certificates from recognized authorities. ISO 14001 addresses environmental management rather than fertilizer approval. It encourages measurable controls for energy, wastewater, dust, emissions, and waste reduction. A strong plant can show inspection logs, corrective actions, and staff training records. Still, paperwork alone does not prove consistent performance.
Tips: Request recent test reports, traceability samples, and audit findings before signing a contract. Visit the plant if possible. Check storage areas, calibration labels, and cleaning routines. Ask who updates regulatory files when rules change. One practical weakness is assuming every certificate covers every product. It often does not. Compare the certificate scope, production site, validity dates, and exact fertilizer type. Keep independent verification in the purchasing process.
„Thanks to the LUVIR technology, the solder resist process could be switched directly from the previously used mask exposure to direct exposure. As an outstanding digital solution on the market, this technology has been able to demonstrate fast process times and superior quality on our certified conventional ink in production. This allowed us to fully digitize the solder mask process at low cost – without process or ink adjustments. An excellent benefit to our production in Rot am See.“
Ralf Göhringer (Head of Production WE Rot am See)
I would definitely recommend the Limata machine and team for a future company purchase
Michael Greenaway
Compunetics Inc.
“The Limata ldi has been amazing!! Best thing we did was buy this machine”
Richard Brady
GM
Circuitlabs
“Since 2019, we have been running the Limata X1000 LDI system (including LUVIR for solder mask imaging) in daily production as an addition to our current process with film. The machine was capable of properly exposing Taiyo PSR-4000 BN (DI) solder mask types on normal to high-copper boards using a new and unique direct imaging process. The machine operating interface is very user friendly which allowed for a quick technical training curve. The pre-registration processing reduced several seconds of production time at every print. Limata support and service staff is incomparable. They supported our team every step of the way at basically any time of the day or night, with literally, an immediate response time, customizing the software interface to best fit our Operations and needs.
We have exposed more than 8,000 prints since end of October, on various solder mask colors and some resist film panels. Limata, has proven to be very capable and innovative. They are a strong contender in the industry.
We have very much enjoyed this project, and working with the team!
Thank you Limata for the continued support and being a part of our growth.”
Bill Sezate
Vice President, GM
Summit Interconnect
As a replacement to our current contact exposure process with film, the LIMATA X2000 system including LUVIR-Technology was capable of properly exposing non-LDI solder mask types using a direct imaging process. The machine offers cutting edge software with a very intuitive operating interface which allowed for quick technician training curve. The dual drawer system combined with pre-registration processing reduced several seconds of production time at every machine cycle. Limata support and service staff is world class. They added software patches to keep production running at shortest possible response times, customized the software interface to best fit our in-house Operations system, and even wrote a step-by-step machine processing manual. As a result of the project, we have exposed more than 16,000 times on various product types and solder mask brands/colors. Limata, in a very short timeframe as a company, has definitely shown they are truly innovative and will be challenging the industry of direct imaging for the top spot.
Kevin Beattie
Process Engineer
TTM Technologies
Forest Grove Division