Choosing the best threaded inserts supplier in China requires more than comparing prices or browsing a polished catalog. Buyers should check whether a supplier understands the insert’s application, base material, thread size, installation method, and expected load. Small details matter. A mismatched knurl pattern or poorly controlled thread can cause problems during assembly. Ask for clear drawings, material specifications, dimensional tolerances, and available inspection records. These details make comparisons more useful than a low quote alone.
Searches for “Inserts Threaded” may lead to manufacturers, trading companies, and specialist exporters. Their capabilities can differ. Ask who makes the parts, what production processes are available, and how changes to a drawing are reviewed. Request samples before placing a large order, then check fit and installation using your actual materials and tools. A supplier’s response to technical questions can reveal as much as the sample itself. Look for direct answers, consistent documentation, and realistic lead times. Very fast promises deserve a closer look.
There is no single supplier that suits every project. One factory may offer broad customization, while another may be stronger in repeat orders or specific insert designs. Even a polished sample cannot prove that every production batch will match it. That is worth remembering. A careful shortlist should balance product quality, communication, production capacity, and support after delivery. With these checks, buyers can approach the search for a dependable Chinese supplier with clearer expectations and fewer surprises.
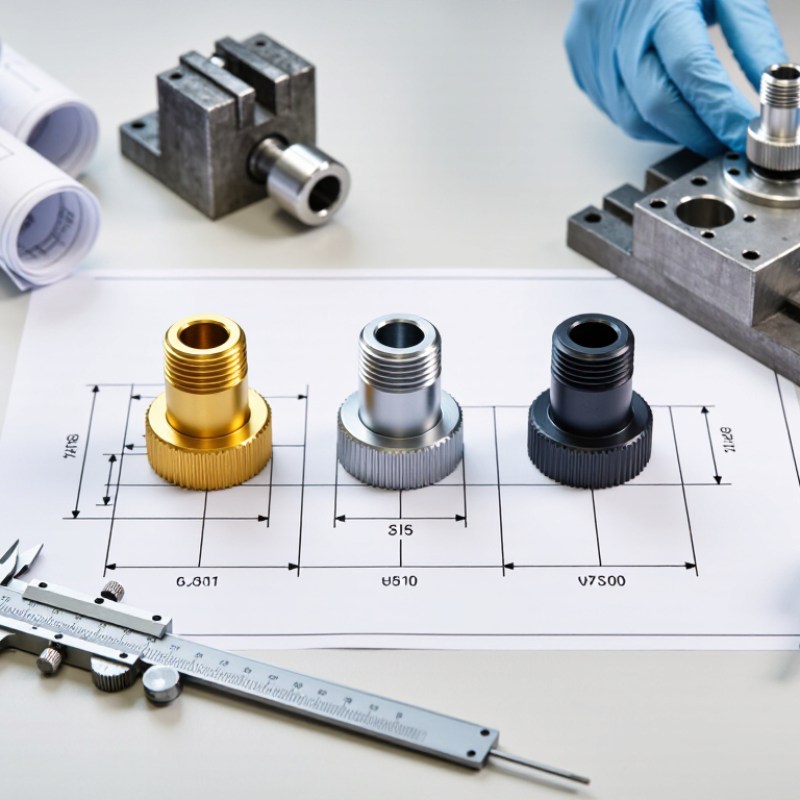
Threaded inserts are metal or plastic components that create durable internal threads in materials that may not hold screws securely. They are commonly used in wood, plastic, and composite panels. An insert can help reduce thread wear when a part is assembled and serviced repeatedly. The right choice depends on the base material, screw size, load, and installation method.
In furniture, inserts can secure legs or removable panels without repeatedly damaging the wood. In plastic housings, they provide stronger fastening points for covers and brackets. Electronics enclosures, vehicle interiors, and industrial equipment may also use them. Design details matter. A knurled exterior can improve grip in some applications, while a smooth insert may suit a different installation process. Oversized holes or poor alignment can still cause failure, so testing in the actual material is important.
Tips: Match the insert to the material and expected load. Check hole size and installation depth. A small sample test can reveal issues before production. It is easy to overlook the material’s variation.
A reliable threaded inserts supplier should be assessed against the actual application, not a broad catalog description. Define the base material, insert type, thread size, installation method, and expected pull-out or torque loads. Include the operating temperature and exposure to moisture or chemicals. Small details matter. For example, an insert fitted into a thin plastic panel may need different knurling and installation controls than one used in an aluminum housing. Share drawings, tolerances, and annual volume estimates before requesting a quote.
Ask how the supplier checks consistency between production lots. Useful evidence may include dimensional inspection records, material documentation, sample results, and a clear method for tracing batches. Request samples for installation trials in the intended material, using the tools and settings your production team will use. Check for thread damage, spinning, cracking, and fit after assembly. Then discuss packaging, lead times, and how changes to dimensions or materials are approved. A requirement list is rarely perfect on day one. Trial results may reveal a tolerance or installation detail that needs revision, so allow room for that conversation. A low unit price is not enough if inspection expectations remain unclear.
Choosing a threaded-insert supplier in China starts with its manufacturing process, not its catalog. Ask how inserts are formed, machined, heat-treated, and finished. A capable factory should explain which operations happen in-house and which are outsourced. That distinction matters. It affects lead time and process control. Request material certificates and ask how incoming wire or bar stock is inspected. For inserts used in plastics, review knurl geometry, installation method, and pull-out or torque test data. For metal assemblies, confirm thread class, tolerances, and inspection gauges. Don’t settle for “we meet the specification.” Ask for sample inspection records linked to the drawing revision.
Tips: Send a drawing that states the material, thread standard, finish, and application temperature. Request pre-production samples and a control plan. Check whether gauges are calibrated and test results match the production lot. A factory video can help, but it cannot replace records.
Production capacity matters too. Review monthly output, changeover time, and how urgent orders are scheduled. Ask for defect and on-time delivery figures, including the reporting period and calculation method. Definitions vary. Verify claims with a pilot order; it can reveal packaging damage, mixed lots, or unclear communication before production scales up. A long machine list looks impressive, but operators, maintenance, and steady inspection routines matter more. Notice how the supplier discusses a failed test. That answer can be more useful than a polished presentation.
A reliable supplier should prove that each insert matches your drawing, material, and application—not just show a polished sample. ISO’s 2022 Survey recorded 1,265,216 ISO 9001 certificates worldwide. That figure indicates broad quality-system adoption, but certification alone does not verify an individual product or production lot. Ask for a current certificate and confirm its issuing body, site, and scope.
Request a sample inspection report covering thread gauges, key dimensions, material, and surface finish. For load-bearing uses, review relevant pull-out or torque test results, including the test method and sample size. Check that batch numbers link reports to actual shipments. A perfect-looking sample can still hide inconsistent production. I would also ask how rejected lots are contained and documented; answers should be specific, not only reassuring.
Tips: Send a drawing with tolerances, then compare measured samples against it. Check the batch. Keep one approved sample for later comparison, and record any inspection gaps before ordering at scale.
Choosing a threaded inserts supplier in China starts with a clear comparison, not the lowest quotation. Share the insert’s material, dimensions, thread type, installation method, and operating conditions. A supplier should explain how its product fits your application, rather than simply confirm availability.
Ask for samples and inspect them against your drawing. Check thread fit with a suitable gauge, then look for burrs, damaged knurls, and inconsistent dimensions. Small details matter. Request material documentation and ask how incoming materials and finished batches are checked. Specific answers are more useful than a polished capability sheet.
Compare suppliers on repeatability, communication, lead time, and packaging, as well as price. Ask whether inspection records can be linked to each production lot. Confirm how changes to drawings or delivery dates are handled. A low unit price may not include sorting, special packing, or freight. In practice, a sample can look perfect while later batches vary, so one inspection is not proof of consistency. It is also easy to overvalue fast replies; clear technical answers matter more. Keep the comparison table simple, but leave room for questions you have not resolved.
Compare supplier test data with relevant material and fastener standards—not just price or lead time.
The bars show minimum tensile strength benchmarks in ISO 898-1 for steel fasteners with nominal diameters up to 16 mm. These are reference values for fastener property classes, not universal threaded-insert ratings. Ask suppliers for insert-specific drawings, material specifications, and test reports before comparing offers.
„Thanks to the LUVIR technology, the solder resist process could be switched directly from the previously used mask exposure to direct exposure. As an outstanding digital solution on the market, this technology has been able to demonstrate fast process times and superior quality on our certified conventional ink in production. This allowed us to fully digitize the solder mask process at low cost – without process or ink adjustments. An excellent benefit to our production in Rot am See.“
Ralf Göhringer (Head of Production WE Rot am See)
I would definitely recommend the Limata machine and team for a future company purchase
Michael Greenaway
Compunetics Inc.
“The Limata ldi has been amazing!! Best thing we did was buy this machine”
Richard Brady
GM
Circuitlabs
“Since 2019, we have been running the Limata X1000 LDI system (including LUVIR for solder mask imaging) in daily production as an addition to our current process with film. The machine was capable of properly exposing Taiyo PSR-4000 BN (DI) solder mask types on normal to high-copper boards using a new and unique direct imaging process. The machine operating interface is very user friendly which allowed for a quick technical training curve. The pre-registration processing reduced several seconds of production time at every print. Limata support and service staff is incomparable. They supported our team every step of the way at basically any time of the day or night, with literally, an immediate response time, customizing the software interface to best fit our Operations and needs.
We have exposed more than 8,000 prints since end of October, on various solder mask colors and some resist film panels. Limata, has proven to be very capable and innovative. They are a strong contender in the industry.
We have very much enjoyed this project, and working with the team!
Thank you Limata for the continued support and being a part of our growth.”
Bill Sezate
Vice President, GM
Summit Interconnect
As a replacement to our current contact exposure process with film, the LIMATA X2000 system including LUVIR-Technology was capable of properly exposing non-LDI solder mask types using a direct imaging process. The machine offers cutting edge software with a very intuitive operating interface which allowed for quick technician training curve. The dual drawer system combined with pre-registration processing reduced several seconds of production time at every machine cycle. Limata support and service staff is world class. They added software patches to keep production running at shortest possible response times, customized the software interface to best fit our in-house Operations system, and even wrote a step-by-step machine processing manual. As a result of the project, we have exposed more than 16,000 times on various product types and solder mask brands/colors. Limata, in a very short timeframe as a company, has definitely shown they are truly innovative and will be challenging the industry of direct imaging for the top spot.
Kevin Beattie
Process Engineer
TTM Technologies
Forest Grove Division