China’s hydraulic equipment market includes manufacturers serving agricultural, construction, industrial, and mobile machinery. For buyers comparing suppliers, the details matter: a ram’s bore, stroke, seals, rod finish, and mounting points must suit the equipment and its working conditions. A polished catalogue is not enough. Ask for material specifications, pressure ratings, inspection records, and clear product drawings. Check how suppliers handle customization, replacement parts, and communication when a component needs review.
Hydraulic Ram Components work together under pressure, so a small mismatch can cause leakage, uneven movement, or premature wear. Cylinder barrels, pistons, rods, seals, and end caps each affect performance. Herbert E. Merritt, author of Hydraulic Control Systems, is a useful reference for understanding hydraulic systems as connected assemblies. A practical principle consistent with that systems perspective is: “Assess each component by how it performs in the complete circuit.” That is a guiding summary, not a verbatim quotation. This article introduces China-based manufacturers and suppliers, with attention to product range, engineering support, quality processes, and buyer checks. Compare evidence, not promises. Ask how dimensions are verified and how finished parts are inspected. Supplier claims still deserve scrutiny, especially when specifications are incomplete. A careful shortlist can help buyers find components suited to real operating demands, rather than choosing on price alone.
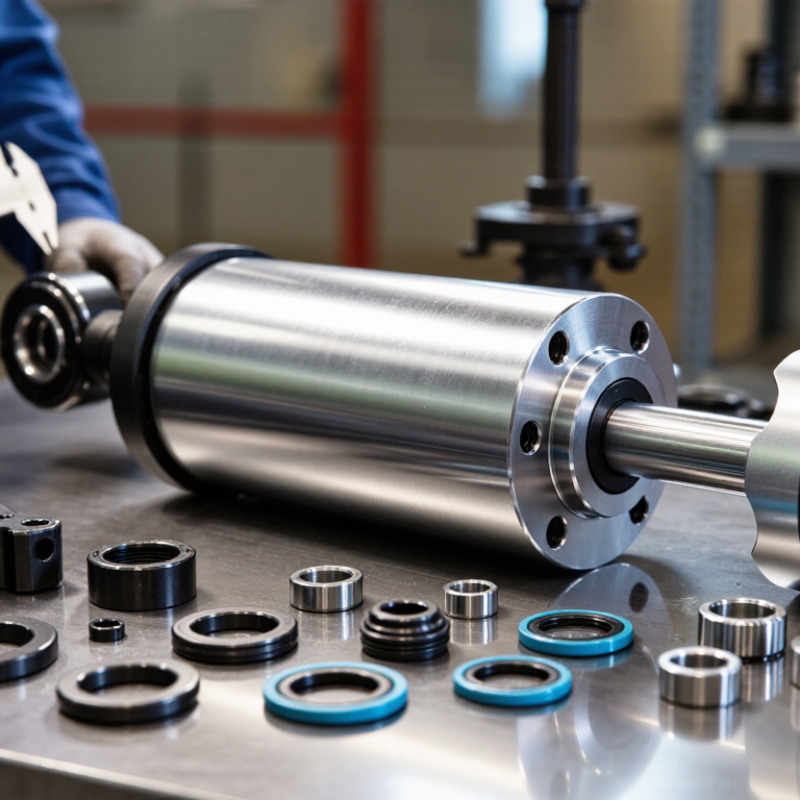
A hydraulic ram converts fluid pressure into straight-line force. Its main parts are a cylinder barrel, piston, rod, seals, ports, and end caps. Pressurized oil enters one side of the piston and pushes the rod outward; reversing or releasing the flow lets the load return. In a workshop, the rod may move only a few centimetres, yet it can lift a heavy fixture. Small parts matter. A scratched rod or worn seal can cause leakage, sluggish motion, or pressure loss.
The U.S. Department of Energy’s Improving Pumping System Performance sourcebook reports that pumping systems use nearly 20% of global electricity and can account for 25–50% of electricity use in some industrial facilities. Those figures describe pumping systems broadly, not hydraulic rams alone, but they underline why matching pump flow and pressure to the actuator matters. For suppliers and equipment builders, check the cylinder bore, stroke, working pressure, seal material, and mounting dimensions against the actual duty cycle. Keep the rod surface clean during inspection. One practical caution: a ram that moves smoothly without a load may still leak internally under load, so a no-load test is not enough.
A hydraulic ram depends on several parts working together under pressure. The cylinder barrel contains the hydraulic fluid and guides the piston through its stroke. Its inner surface needs a consistent finish; scratches can wear seals and cause leakage. The piston separates pressure zones inside the barrel. Small details matter.
The piston rod transfers force to the load. It should resist bending and have a smooth, protected surface where it passes through the gland. Seals around the piston and rod limit fluid loss and help keep dirt out. Their material and shape must suit the fluid, temperature, and operating pressure. A seal that fits poorly may fail early, even when the metal parts look sound. That mismatch is easy to overlook.
End caps close the cylinder, while the gland supports the rod and often holds its seals and wiper. Ports direct fluid into and out of the ram; their position affects hose routing and installation space. Some designs include cushioning near the stroke ends to reduce impact. During inspection, check dimensions, surface condition, and seal seating, not just appearance. A tidy assembly is reassuring, but it does not prove reliable performance. Testing under suitable conditions still matters.
Standard nominal pressure ratings for selected hydraulic cylinder series
ISO 6020-1 and ISO 6020-2 cylinder series have a 16 MPa nominal pressure rating; the ISO 6022 series is rated at 25 MPa. These ratings provide context for designing core ram components—including the barrel, piston, rod, seals, and end caps—to suit the cylinder’s intended pressure. Source: ISO 6020-1, ISO 6020-2, and ISO 6022.
China’s hydraulic ram component manufacturing landscape spans metal forming, precision machining, tube processing, and seal production. Suppliers often specialize in particular steps rather than making every part in-house. A cylinder barrel may be honed for a consistent bore, while a piston rod receives surface treatment to resist wear and corrosion. Small details matter.
Production capabilities vary between regions and factories. Some workshops handle custom dimensions and small batches; larger operations may offer repeatable machining and inspection processes. Buyers can assess practical evidence: material certificates, dimensional reports, pressure-test records, and clear drawings. Ask how bore diameter, rod straightness, and surface finish are checked, not just whether a factory has modern equipment. Those checks can reveal process discipline.
The supply base is broad, but consistency is not automatic. A sample may look sound and still differ from later production if process controls are weak. That gap matters. Communication also deserves attention: unclear tolerances or changing specifications can create delays and rework. It is sensible to confirm operating pressure, stroke, mounting dimensions, and fluid compatibility before production begins. No checklist removes every risk, and smaller suppliers may have limited testing capacity. Buyers should match inspection depth to the component’s duty and expected service life.
A reliable hydraulic ram component supplier should prove performance with traceable test records, not polished catalogues alone. Ask for material certificates, heat-treatment results, dimensional inspection sheets, and pressure-test data for the exact part number. For a piston rod, check coating thickness, surface finish, and straightness; for seals, request compound identification and temperature limits. Compare samples against your drawings, then confirm that production parts follow the same inspection plan. Small details matter.
Use recognized measurement frameworks. ISO 4406:2021 classifies hydraulic-fluid cleanliness by particle counts, so specify a cleanliness target and ask how components are protected from contamination during machining, washing, and packing. The World Bank’s 2023 Logistics Performance Index scored China 3.7 out of 5 overall. That national score is useful context, not proof that an individual supplier ships reliably. Review the supplier’s own on-time delivery history, packaging photos, and corrective-action records. Ask for recent examples.
A factory visit can reveal whether gauges are calibrated and whether rejected parts are physically separated. Remote audits help, but they miss habits on the shop floor. One imperfect point: a supplier may have strong certificates yet weak process control on a new design. Start with a pilot order, define measurable acceptance limits, and retain samples from each batch. Independent testing costs time. It may prevent a costly hydraulic failure later.
For China Top Hydraulic Ram Components Manufacturers and Suppliers, sourcing should begin with the operating conditions, not the lowest quotation. Specify working pressure, load cycles, temperature range, fluid type, and connection dimensions. Ask suppliers to identify the steel grade, heat-treatment process, and sealing material. For each batch, request material certificates, dimensional inspection records, and pressure-test results linked to traceable lot numbers. A neat certificate is useful; a verifiable production record is better.
Quality checks should cover more than visible finish. ISO 4406:2021 classifies hydraulic-fluid cleanliness using particle counts at 4, 6, and 14 micrometres. For example, code 18 represents 1,300–2,500 particles per millilitre at a given size threshold. This is a measurement reference, not a universal acceptance target; confirm limits against the component and system requirements. Check whether suppliers document test equipment calibration and follow ISO 4413 design principles for hydraulic systems. Small gaps in records can become expensive.
Tips: Request a sample inspection and review its raw test data. Compare drawing revisions carefully. I have seen sourcing plans overlook this simple step. Then ask how nonconforming parts are isolated and corrected.
„Thanks to the LUVIR technology, the solder resist process could be switched directly from the previously used mask exposure to direct exposure. As an outstanding digital solution on the market, this technology has been able to demonstrate fast process times and superior quality on our certified conventional ink in production. This allowed us to fully digitize the solder mask process at low cost – without process or ink adjustments. An excellent benefit to our production in Rot am See.“
Ralf Göhringer (Head of Production WE Rot am See)
I would definitely recommend the Limata machine and team for a future company purchase
Michael Greenaway
Compunetics Inc.
“The Limata ldi has been amazing!! Best thing we did was buy this machine”
Richard Brady
GM
Circuitlabs
“Since 2019, we have been running the Limata X1000 LDI system (including LUVIR for solder mask imaging) in daily production as an addition to our current process with film. The machine was capable of properly exposing Taiyo PSR-4000 BN (DI) solder mask types on normal to high-copper boards using a new and unique direct imaging process. The machine operating interface is very user friendly which allowed for a quick technical training curve. The pre-registration processing reduced several seconds of production time at every print. Limata support and service staff is incomparable. They supported our team every step of the way at basically any time of the day or night, with literally, an immediate response time, customizing the software interface to best fit our Operations and needs.
We have exposed more than 8,000 prints since end of October, on various solder mask colors and some resist film panels. Limata, has proven to be very capable and innovative. They are a strong contender in the industry.
We have very much enjoyed this project, and working with the team!
Thank you Limata for the continued support and being a part of our growth.”
Bill Sezate
Vice President, GM
Summit Interconnect
As a replacement to our current contact exposure process with film, the LIMATA X2000 system including LUVIR-Technology was capable of properly exposing non-LDI solder mask types using a direct imaging process. The machine offers cutting edge software with a very intuitive operating interface which allowed for quick technician training curve. The dual drawer system combined with pre-registration processing reduced several seconds of production time at every machine cycle. Limata support and service staff is world class. They added software patches to keep production running at shortest possible response times, customized the software interface to best fit our in-house Operations system, and even wrote a step-by-step machine processing manual. As a result of the project, we have exposed more than 16,000 times on various product types and solder mask brands/colors. Limata, in a very short timeframe as a company, has definitely shown they are truly innovative and will be challenging the industry of direct imaging for the top spot.
Kevin Beattie
Process Engineer
TTM Technologies
Forest Grove Division