Choosing a finish for a die-cast component is not a cosmetic decision. It affects corrosion resistance, coating adhesion, electrical contact, appearance, and the cost of every production run. A bright, even surface may suit a visible appliance housing, while a conversion coating may better serve a part exposed to moisture. The right choice depends on alloy, geometry, operating conditions, and the buyer’s acceptance criteria.
The scale of the market makes this decision consequential. Grand View Research estimated the global die casting market at USD 82.7 billion in 2023 and projected a 6.2% compound annual growth rate from 2024 to 2030. That figure covers die casting broadly, not finishing alone. For practical requirements, buyers can consult NADCA’s Product Specification Standards for Die Castings and request sample parts before approving a process. Look closely at recessed corners, machined faces, and edges where coating thickness can vary. Small details matter.
Die Cast Part Surface Finishing options include conversion coatings, powder coating, wet painting, plating, and mechanical treatments. Each brings trade-offs in cost, appearance, protection, and dimensional impact. One limitation deserves candor: I could not verify a direct quotation from a named finishing specialist, so I have not invented one. Treat broad market forecasts as context, not proof that a particular finish will perform. Ask suppliers for documented process limits, test results, and parts finished on the same alloy and geometry. A sample can still mislead. Production variation needs review.
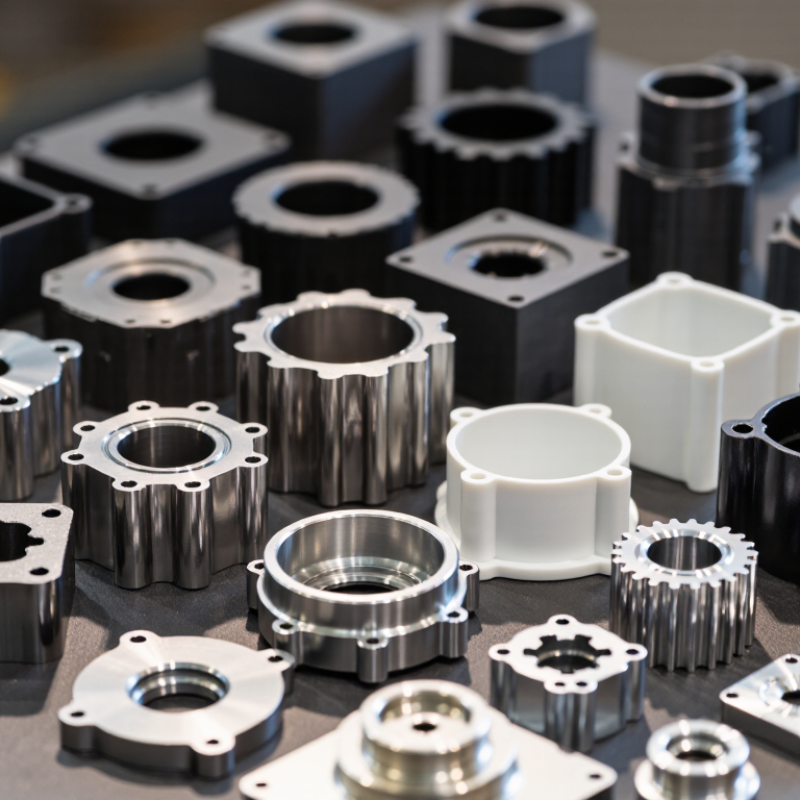
Surface finishing changes how a die cast part performs, feels, and holds up in use. A conversion coating or paint layer can slow corrosion and reduce staining, while powder coating adds a thicker, durable surface. Polishing can make visible faces smoother, but it may also reveal small pits that were less obvious on the raw casting. Small details matter. A finish can improve grip, cleanability, or appearance, depending on the part’s job.
The choice should match the alloy, environment, and required dimensions. For example, a housing used outdoors may need corrosion protection, while a component with close-fitting holes may require masking during coating. Finishing adds thickness, so fit and tolerance checks should happen before production approval. It does not repair internal porosity or poor casting quality.
Not always. A premium finish may add cost without improving a hidden component.
Ask for sample parts, inspect edges and recesses, and confirm that the process produces consistent coverage. One practical caution: a perfect-looking sample does not guarantee every production batch will look identical. The specification should define acceptable color, texture, and visible defects.
Before selecting a die cast surface finish, define what the part must do and what users will see. A handled housing may need consistent color and resistance to fingerprints. A hidden bracket may prioritize corrosion protection and fit over gloss. Be specific. Record the alloy, casting condition, machined areas, expected environment, and any contact with seals or fasteners.
Translate those details into measurable acceptance criteria. State visible zones, allowable texture variation, color range, coating thickness, and inspection method. For a mating face, set a roughness or flatness limit and mask it if coating could affect assembly. For outdoor use, describe moisture, cleaning chemicals, and temperature exposure instead of asking for a “durable” finish. That word is vague. Approve a sample under the same lighting used for inspection; color can look different in a workshop.
Keep performance and appearance requirements separate, then check where they conflict. A thicker coating may improve coverage but alter holes or edges. Polishing can brighten a surface while revealing porosity. It is easy to overreact to a small cosmetic mark and overlook a functional edge condition. That deserves a second look. Agree on defect limits, document the approved sample, and revisit the criteria after pilot parts reveal process variation.
Die-cast parts can be finished in several ways, depending on their alloy, shape, and working environment. Powder coating creates a durable, even layer and suits housings or brackets that need color. Wet paint can cover complex shapes, though careful cleaning and curing matter. Plating gives zinc parts a bright, metallic appearance, while conversion coatings can improve corrosion resistance or paint adhesion. Bead blasting creates a uniform matte texture, but it does not protect the surface by itself.
Tips: Confirm the alloy before choosing a finish. Ask for sample parts when color or texture matters. Check edges, holes, and recessed areas; coating thickness may vary there.
Surface preparation is easy to underestimate. Trapped release agent, pores, or sharp edges can cause poor adhesion or visible defects. Anodizing may work on some aluminum die castings, but silicon content and alloy composition can affect the result. It is not a universal choice. A supplier should review the part drawing and intended use before recommending a process. Even then, finish samples may differ slightly from production parts, so set realistic appearance limits.
Typical coating thickness ranges for common die cast part finishes
Thickness ranges are typical reference values, not universal specifications. Actual results vary by alloy, part geometry, preparation, and finishing requirements. Anodizing is applicable only to suitable aluminum alloys; die cast alloys may produce variable results.
Material and part design shape the finish long before a coating is applied. Aluminum die castings are lightweight, but their silicon content and surface porosity can make decorative anodizing less consistent. A conversion coating or powder coat may provide more predictable coverage. Zinc alloys often support smooth plating, though thin walls and small features need careful handling. Magnesium requires a compatible pretreatment to help coatings adhere.
Geometry matters just as much. Deep recesses can trap pretreatment chemicals, while sharp edges may receive thinner coating coverage. Ribs, narrow slots, and draft angles can complicate polishing or blasting. For example, a textured powder coat can hide minor surface variation on a broad housing, but it may soften fine lettering. Ask for sample parts made with the intended alloy and tooling. A finish that looks even on a flat test panel may behave differently around bosses and corners. I have seen specifications focus on color, then overlook masking locations and coating buildup.
Tips: Share the alloy, drawing, and critical dimensions with your finisher. Mark surfaces that need masking or tight tolerances. Request a sample from production tooling, and inspect both visible faces and recessed areas. Be ready to revise the finish if the first trial exposes weak spots.
Choosing a die cast finish starts with the part’s job, not its appearance. A decorative indoor housing may need only a smooth, consistent coating. An outdoor bracket faces moisture, handling, and temperature changes. Powder coating can provide a tough, opaque layer, but sharp edges and deep recesses may receive uneven coverage. Check sample parts from the actual casting process. A polished prototype can hide porosity that appears later.
Compare total production cost, not just the quoted finish price. Include cleaning, surface preparation, masking, inspection, and expected rework. Plating can create a bright, durable surface, yet casting pores may cause defects unless preparation is controlled. Anodizing is not equally predictable across all die cast alloys. Ask the supplier to confirm alloy compatibility and show finished production samples. Small details matter.
Durability claims need context. A salt-spray result does not guarantee years of service in every environment. Match testing to real exposure, including abrasion, cleaning chemicals, and contact with other components. For high-volume runs, consider line speed, rack space, color consistency, and how easily defects can be detected. It depends. A finish that looks premium on one sample may be costly at scale. Sometimes, a simpler coating with clear acceptance criteria is the safer choice.
| Finish option | Appearance and surface effect | Relative cost | Durability and protection | Production fit | Best suited for | Buyer considerations |
|---|---|---|---|---|---|---|
| As-cast with basic trimming | Retains the die-cast texture and visible parting-line or gate-removal marks; appearance varies with tooling and process control. | Low | Provides no added coating protection. Performance depends on the alloy and service environment. | Fastest option; avoids a separate coating line. | Internal components, concealed parts, and applications where appearance or added corrosion protection is not critical. | Agree on acceptable surface variation, flash, and gate-removal marks. Specify any cosmetic zones separately. |
| Vibratory or tumble deburring | Removes small burrs and can soften sharp edges; typically leaves a uniform, matte surface rather than a high-gloss finish. | Low to moderate | Improves edge condition but does not provide a corrosion-resistant coating. | Suitable for batch processing and repeat production; part geometry must allow media to reach relevant areas. | Parts needing smoother edges before assembly, handling, or a later coating step. | Confirm that media will not damage thin features, critical dimensions, threads, or precision surfaces. |
| Bead blasting | Creates a consistent matte or satin appearance and can reduce the visual contrast of minor surface irregularities. | Low to moderate | Does not add a protective film; blasted surfaces may need prompt coating where corrosion is a concern. | Can be used as a standalone cosmetic step or as surface preparation before painting or powder coating. | Decorative housings and parts requiring a uniform, non-glossy surface. | Specify media, pressure, and masking requirements. Blasting does not remove major casting defects. |
| Powder coating | Provides a broad range of colors and gloss levels with a relatively thick, continuous film. | Moderate | Generally offers good abrasion and corrosion protection when the surface is properly pretreated and the coating is correctly cured. | Well suited to repeat production; curing requires a compatible oven cycle and adequate part fixturing. | Exterior housings, brackets, and parts needing durable color and a substantial protective layer. | Check cure-temperature compatibility, coating thickness at edges and recesses, masking needs, and possible gas release from porous castings. |
| Wet paint | Allows a wide choice of colors, gloss levels, and visual effects; can be applied in relatively controlled film thicknesses. | Moderate; varies by coating system and application method | Protection depends on the paint chemistry, film build, pretreatment, and exposure conditions. | Flexible for different part sizes and lower-volume color changes; drying or curing time affects throughput. | Parts requiring specific colors, visual effects, or a finish that is difficult to achieve with powder coating. | Define the paint system and required performance. Include surface preparation, masking, and handling in the cost comparison. |
| Conversion coating | Usually produces a thin, clear or lightly colored surface with little change to part dimensions. | Low to moderate | Can improve corrosion resistance and paint adhesion, but is generally less protective as a standalone finish than a substantial paint or powder film. | Often used as a pretreatment before painting or powder coating; process suitability depends on the alloy and specification. | Parts needing a thin pretreatment layer or a base for a subsequent coating. | Confirm the coating chemistry, alloy compatibility, and required test standard. Do not assume all conversion coatings provide the same protection. |
| Electroplating | Can provide a metallic appearance, including bright or satin finishes, depending on the plating system. | Moderate to high | Protection and wear performance depend on the substrate, underlayers, deposit thickness, and plating system. | Requires controlled cleaning and pretreatment; production timing includes multiple process stages. | Decorative or functional parts needing a metallic surface, subject to suitable substrate and process design. | Specify the base alloy, plating stack, thickness, and acceptance criteria. Die-cast porosity and surface defects can affect appearance and coating integrity. |
| Anodizing (aluminum alloys) | Forms an oxide layer and can create a range of colors; results depend strongly on alloy composition and surface condition. | Moderate to high | Can improve surface wear and corrosion performance when the alloy and anodizing process are suitable. | Requires alloy-specific process control and consistent pretreatment; cosmetic consistency can be challenging across some die-cast alloys. | Selected aluminum die-cast parts where the alloy is compatible and the appearance has been validated on production samples. | Do not assume every aluminum die-cast alloy anodizes uniformly. Confirm alloy suitability and approve representative samples before release. |
Comparison note: Relative cost and production fit are general planning guides, not quotations. Actual results depend on part geometry, alloy, surface condition, coating specification, batch size, masking, and inspection requirements. Validate cosmetic finishes and performance requirements using samples from the intended production process.
„Thanks to the LUVIR technology, the solder resist process could be switched directly from the previously used mask exposure to direct exposure. As an outstanding digital solution on the market, this technology has been able to demonstrate fast process times and superior quality on our certified conventional ink in production. This allowed us to fully digitize the solder mask process at low cost – without process or ink adjustments. An excellent benefit to our production in Rot am See.“
Ralf Göhringer (Head of Production WE Rot am See)
I would definitely recommend the Limata machine and team for a future company purchase
Michael Greenaway
Compunetics Inc.
“The Limata ldi has been amazing!! Best thing we did was buy this machine”
Richard Brady
GM
Circuitlabs
“Since 2019, we have been running the Limata X1000 LDI system (including LUVIR for solder mask imaging) in daily production as an addition to our current process with film. The machine was capable of properly exposing Taiyo PSR-4000 BN (DI) solder mask types on normal to high-copper boards using a new and unique direct imaging process. The machine operating interface is very user friendly which allowed for a quick technical training curve. The pre-registration processing reduced several seconds of production time at every print. Limata support and service staff is incomparable. They supported our team every step of the way at basically any time of the day or night, with literally, an immediate response time, customizing the software interface to best fit our Operations and needs.
We have exposed more than 8,000 prints since end of October, on various solder mask colors and some resist film panels. Limata, has proven to be very capable and innovative. They are a strong contender in the industry.
We have very much enjoyed this project, and working with the team!
Thank you Limata for the continued support and being a part of our growth.”
Bill Sezate
Vice President, GM
Summit Interconnect
As a replacement to our current contact exposure process with film, the LIMATA X2000 system including LUVIR-Technology was capable of properly exposing non-LDI solder mask types using a direct imaging process. The machine offers cutting edge software with a very intuitive operating interface which allowed for quick technician training curve. The dual drawer system combined with pre-registration processing reduced several seconds of production time at every machine cycle. Limata support and service staff is world class. They added software patches to keep production running at shortest possible response times, customized the software interface to best fit our in-house Operations system, and even wrote a step-by-step machine processing manual. As a result of the project, we have exposed more than 16,000 times on various product types and solder mask brands/colors. Limata, in a very short timeframe as a company, has definitely shown they are truly innovative and will be challenging the industry of direct imaging for the top spot.
Kevin Beattie
Process Engineer
TTM Technologies
Forest Grove Division
