Buying a Cnc Aluminum Profile worldwide is not simply a price comparison. It is a technical sourcing decision.
The global aluminum extrusion market continues to expand through construction, automation, transport, and renewable energy. Grand View Research estimates that the market will grow steadily through 2030. The International Aluminium Institute also reports annual global aluminum production above 70 million tonnes. These figures suggest strong supply capacity. They do not guarantee consistent quality.
A buyer still needs to inspect alloy, temper, dimensional tolerance, surface finish, and packaging. A profile may look identical on a screen. Its wall thickness can differ by fractions of a millimeter. That difference may affect assembly, vibration, and load performance. Ask for mill certificates, inspection records, sample sections, and clear tolerance tables. ISO 9001 certification helps, but it never replaces product verification.
Charles M. Johnson Jr., President and CEO of The Aluminum Association, has stated, “Aluminum is a critical material for our economy and national security.” His point also applies to international sourcing. Material availability, recycling, energy use, and supply-chain resilience deserve attention.
This guide presents 10 practical tips for buying Cnc Aluminum Profile worldwide. It covers supplier audits, alloy selection, quotation checks, tooling costs, shipping protection, and after-sales support. Some recommendations may seem obvious. They are often missed under deadline pressure.
One honest limitation remains. No checklist can remove every sourcing risk. A low-cost supplier may become expensive after rework, delays, or rejected batches. Careful documentation feels slower at the beginning. It usually saves time later.
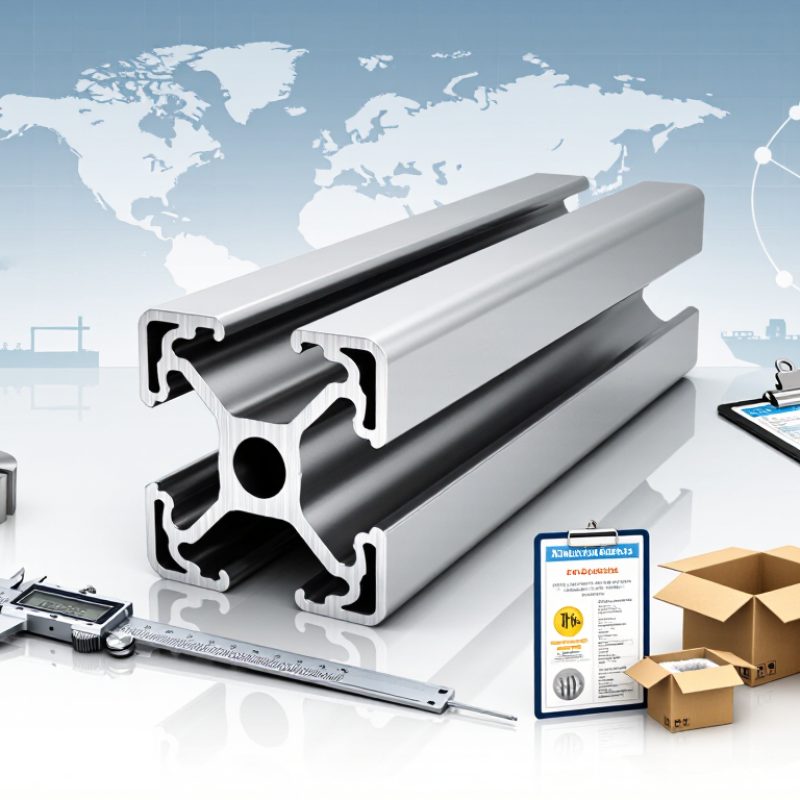
CNC aluminum profiles are extruded aluminum sections shaped or machined with computer-controlled equipment. Their form usually begins with a standard cross-section, such as a T-slot rail, frame beam, or curved housing. CNC operations then add precise holes, pockets, threads, and cutouts. This combination reduces manual fitting during assembly. It also supports repeatable production across international suppliers.
These profiles appear in machine guards, robotic frames, lighting structures, laboratory equipment, and lightweight transport fixtures. Aluminum offers useful corrosion resistance and a strong strength-to-weight ratio. However, alloy selection still matters. A rigid support may require a different alloy from a decorative panel. Surface treatment also changes performance. Anodizing can improve appearance and wear resistance, while powder coating provides more color choices. Ask for dimensional tolerances, alloy certificates, inspection records, and sample parts before ordering large quantities.
In practical sourcing, I compare the CAD drawing with the finished profile, not only the supplier’s quotation. Check hole positions, thread depth, flatness, and edge quality. Small errors can become expensive when several frames must align. Packaging deserves attention too; long profiles can bend during overseas transport. I once underestimated this risk and focused too much on machining accuracy. The parts were precise, but several arrived with damaged corners. That mistake changed my inspection checklist. A profile may look perfect on a screen. Real applications are less forgiving.
Defining Technical Requirements Before Purchasing
Buying CNC aluminum profiles worldwide starts with a clear technical brief, not a supplier comparison. Record the alloy, temper, profile dimensions, wall thickness, cut length, and required tolerances. Specify the load, span, vibration, and mounting method. A profile supporting a light guard differs greatly from one carrying a moving assembly.
Tip 1: Draw the application.
Include hole positions, machining depths, thread types, and critical reference surfaces. State whether the finish is natural, anodized, or powder-coated. Also define acceptable scratches, color variation, and burr limits. These details prevent different factories from interpreting “high quality” in different ways. Request material certificates and dimensional inspection records when traceability matters. They are useful, but they do not replace checking samples.
Tip 2: Test before scaling.
Order a small sample with the same machining and finish as production parts. Measure it with calibrated tools, then assemble it under realistic conditions. Check fit, straightness, surface damage, and thread strength. Packaging deserves attention too. Long profiles can bend when poorly supported during international transport.
I have seen an excellent extrusion arrive unusable because the crate allowed movement. That mistake was avoidable.
Leave room for revision. Your first drawing may miss drainage, tool clearance, or access for maintenance. Ask a qualified engineer to review stress points and tolerance stacks before approval. Confirm packing dimensions, delivery terms, inspection timing, and document requirements in writing. Clear requirements reduce disputes, waste, and expensive rework.
Buying CNC aluminum profiles worldwide requires more than comparing unit prices. Supplier capability matters.
Tip 1: Verify extrusion and CNC equipment lists. Ask for machine sizes, axis counts, tolerance ranges, and maintenance records. Tip 2: Request recent inspection reports, not promotional photos. Tip 3: Check whether one facility controls extrusion, aging, cutting, machining, and packing. Fewer transfers usually reduce damage and dimensional variation. The International Aluminium Institute reported global primary aluminum production of about 70.6 million tonnes in 2023. Large output does not guarantee stable profile quality. Material traceability still matters. Tip 4: Require alloy certificates and heat numbers for every batch. Tip 5: Confirm temper, surface treatment, and profile straightness before sampling.
Tip 6: Send a detailed drawing with datums, hole locations, thread standards, and acceptable burr limits. Tip 7: Test a pilot lot before signing annual volumes. Measure critical features with calibrated equipment. Tip 8: Review the supplier’s corrective-action process. A polished sample can hide weak production control. I have seen buyers focus on machining speed and overlook packaging strength. That mistake becomes expensive after ocean transport. Tip 9: Compare logistics performance, customs experience, and export documentation. The World Bank’s 2023 Logistics Performance Index evaluates 139 economies, including customs, infrastructure, and shipment reliability. Use those indicators as context, not proof. Tip 10: Define inspection ownership, replacement rules, and delivery penalties in writing. Also confirm production capacity during peak months. Capacity claims are often optimistic. A factory visit, video audit, or independent inspection can expose the difference.
10 Tips for Buying CNC Aluminum Profiles Worldwide
Comparing materials is more useful than choosing the lowest quote. Aluminum 6063 usually offers clean extrusion surfaces and reliable anodizing results. Aluminum 6061 provides higher strength, but machining may cost more. Confirm the temper, alloy certificate, dimensional tolerance, and intended load before requesting prices. A profile can look identical while performing differently. Small details matter.
Finish affects both appearance and durability. Mill finish is economical, but it may show die lines and minor color variation. Anodizing improves corrosion resistance and creates a consistent surface, though shade matching needs approved samples. Powder coating offers many colors, but thick coating can affect tight assembly points. Ask for coating thickness, color tolerance, and protected packaging. Scratched profiles are expensive to rework.
Compare prices using the landed cost, not only the unit price. Include tooling, CNC setup, finishing, inspection, packing, freight, and possible sample charges. Minimum order quantities vary widely. A low MOQ may carry a higher piece price, while a large order can create excess stock. Request a trial batch when tolerances are critical. It exposes problems early. Still, trial batches are not perfect; production behavior can change with different billet lots or machine settings. Confirm how replacements, inspection records, and delivery changes will be handled before placing the order.
Checking Quality Standards, Shipping Terms, and Import Duties
1) Specify the alloy, temper, dimensions, and tolerance before requesting prices.
2) Ask for mill certificates, inspection records, and surface-finish samples.
3) Match testing requirements with recognized standards, such as ISO 9001 processes and applicable EN or ASTM specifications. Certification alone proves little.
4) Require a first-article inspection for complex channels, drilled holes, or tight tolerances. Small profile distortions can disrupt assembly.
5) Confirm the exact HS classification, often within heading 7604 for aluminum profiles. Ask your customs broker to verify it before payment. The WTO World Tariff Profiles report shows that duty treatment varies by economy and product line.
6) Calculate duty, VAT, brokerage, and port charges separately. A low factory price may hide expensive landed costs.
7) Compare Incoterms carefully, especially EXW, FOB, and DDP. DDP may simplify delivery, but documentation and tax control require scrutiny.
8) Check whether the invoice, packing list, certificate of origin, and bill of lading use matching descriptions.
9) Review transit time and cargo protection. UNCTAD’s Review of Maritime Transport 2023 states that over 80% of global merchandise trade by volume moves by sea. Long voyages need dry packaging, edge protection, and corrosion prevention.
10) Track the supplier’s delivery performance, not only quoted lead time. The World Bank’s 2023 Logistics Performance Index compares 139 economies across customs, tracking, infrastructure, and timeliness. These indicators help, but they cannot replace a sample inspection. I would still budget for delays. Real shipments rarely behave perfectly.
„Thanks to the LUVIR technology, the solder resist process could be switched directly from the previously used mask exposure to direct exposure. As an outstanding digital solution on the market, this technology has been able to demonstrate fast process times and superior quality on our certified conventional ink in production. This allowed us to fully digitize the solder mask process at low cost – without process or ink adjustments. An excellent benefit to our production in Rot am See.“
Ralf Göhringer (Head of Production WE Rot am See)
I would definitely recommend the Limata machine and team for a future company purchase
Michael Greenaway
Compunetics Inc.
“The Limata ldi has been amazing!! Best thing we did was buy this machine”
Richard Brady
GM
Circuitlabs
“Since 2019, we have been running the Limata X1000 LDI system (including LUVIR for solder mask imaging) in daily production as an addition to our current process with film. The machine was capable of properly exposing Taiyo PSR-4000 BN (DI) solder mask types on normal to high-copper boards using a new and unique direct imaging process. The machine operating interface is very user friendly which allowed for a quick technical training curve. The pre-registration processing reduced several seconds of production time at every print. Limata support and service staff is incomparable. They supported our team every step of the way at basically any time of the day or night, with literally, an immediate response time, customizing the software interface to best fit our Operations and needs.
We have exposed more than 8,000 prints since end of October, on various solder mask colors and some resist film panels. Limata, has proven to be very capable and innovative. They are a strong contender in the industry.
We have very much enjoyed this project, and working with the team!
Thank you Limata for the continued support and being a part of our growth.”
Bill Sezate
Vice President, GM
Summit Interconnect
As a replacement to our current contact exposure process with film, the LIMATA X2000 system including LUVIR-Technology was capable of properly exposing non-LDI solder mask types using a direct imaging process. The machine offers cutting edge software with a very intuitive operating interface which allowed for quick technician training curve. The dual drawer system combined with pre-registration processing reduced several seconds of production time at every machine cycle. Limata support and service staff is world class. They added software patches to keep production running at shortest possible response times, customized the software interface to best fit our in-house Operations system, and even wrote a step-by-step machine processing manual. As a result of the project, we have exposed more than 16,000 times on various product types and solder mask brands/colors. Limata, in a very short timeframe as a company, has definitely shown they are truly innovative and will be challenging the industry of direct imaging for the top spot.
Kevin Beattie
Process Engineer
TTM Technologies
Forest Grove Division