Global warehouses rarely share the same operating conditions. One facility may handle cartons on narrow aisles, while another moves heavy pallets across several shifts. An Automatic Stacker can support vertical storage and material movement, but the right model depends on the work it must perform. Capacity matters. So do load dimensions, lift height, aisle width, floor condition, and the speed of daily order cycles. These details sound ordinary. They often decide whether equipment fits the operation or becomes a constraint.
This guide explains how to compare stacker types, review key specifications, and assess integration with existing warehouse systems. Start with actual load data and traffic patterns, not a brochure’s headline figures. Ask suppliers about rated capacity at the required lift height, operator training, service access, and spare-part availability. Request a site assessment where possible. Check how the machine behaves around racking, charging areas, and pedestrian routes. A technically suitable unit may still be a poor fit if maintenance is difficult or staff cannot use it confidently. That deserves a second look. Real operating costs can also differ from initial estimates, especially when duty cycles are misjudged. The following sections offer a practical framework for making a measured choice, while recognizing that no single configuration suits every warehouse. A few assumptions may need revisiting once real site measurements are available.
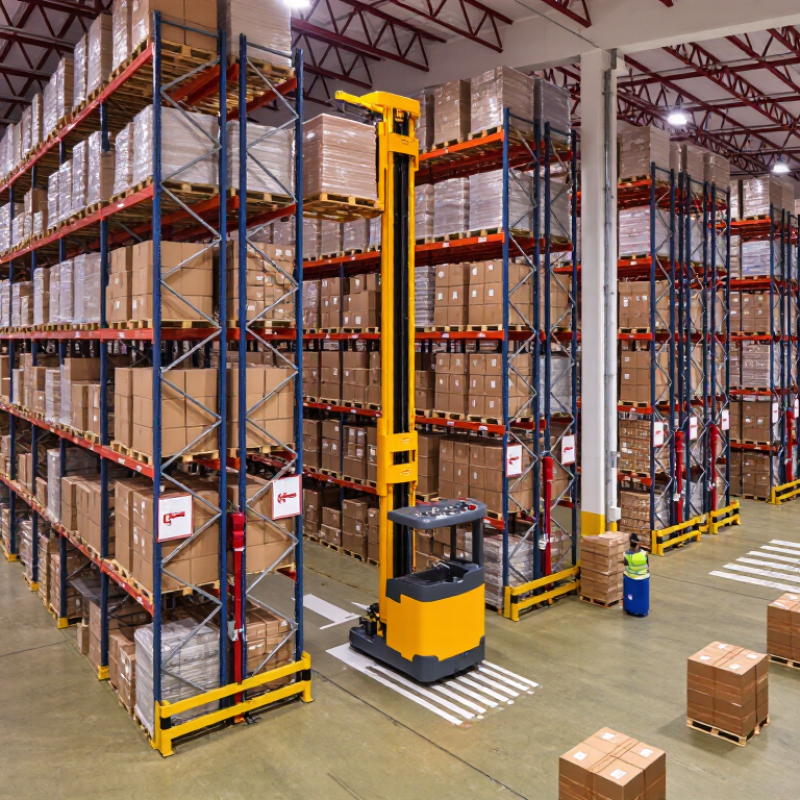
An automatic stacker is a powered machine that lifts and moves pallets or loads between storage locations. In a high-bay warehouse, the term often describes a stacker crane running along a fixed aisle. It travels on floor rails, rises on a mast, and uses forks or a shuttle to transfer loads to racks. Some facilities use “automatic stacker” for a different machine, so check the equipment’s intended task before comparing systems.
The process begins when warehouse software assigns a storage or retrieval task. A control system sends the destination to the stacker, which follows its aisle and uses sensors to position itself at the correct rack level. Forks then extend, place or collect the pallet, and return it to a conveyor or transfer point. Barcode or RFID scans can verify load identity. Small errors matter: a damaged pallet or incorrect load data may interrupt the cycle.
Automation is expanding, but that does not make every warehouse a fit. MHI’s 2024 Annual Industry Report found that 55% of surveyed supply-chain professionals planned to invest more than $1 million in supply-chain innovation over the next two years. The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023; this broader figure signals adoption, not stacker demand. Before choosing a system, check aisle dimensions, pallet consistency, throughput peaks, and maintenance access. A fast machine can still wait on a blocked transfer point.
An automatic stacker should fit the work your warehouse actually handles, not just its floor plan. Start with load weight, pallet dimensions, and the highest storage level. Then measure aisle width, turning space, floor condition, and any ramps or uneven joints. A stacker that clears a drawing may still struggle around a busy corner. Small details matter.
Daily volume and shift patterns help define the required operating pace. Consider how often the machine will move, how long it must run between charging periods, and whether staff need time for routine checks. Dust, temperature changes, and narrow transfer points can also affect performance. Check that the stacker can connect safely with existing equipment and that operators can see clearly around loads. That part is easy to overlook. Site measurements and a practical trial can expose problems before a purchase; specifications alone may not capture a real shift. There is no perfect checklist, and early assumptions sometimes need revisiting. Include maintenance access, spare-part availability, and operator training in the decision, especially across multiple warehouse locations.
Automatic stackers differ in how they move, lift, and handle pallets. Walk-behind electric models suit short routes and lower lift heights, but operators still guide every trip. Ride-on stackers cover longer runs with less walking. Autonomous stackers can follow mapped routes and repeat pallet transfers, though they need reliable navigation, safe crossings, and carefully prepared floors. Small details matter: a chipped pallet or reflective floor can disrupt consistent sensing.
Features should match the warehouse, not just its peak throughput. Compare rated capacity at the required lift height, turning radius, aisle width, battery runtime, charging method, and performance in cold or dusty zones. Straddle designs accommodate varied pallet widths; counterbalance models avoid front support legs but require more clearance. A compact unit may fit an aisle yet struggle with uneven joints. That trade-off is easy to miss.
The International Federation of Robotics reported 4.28 million industrial robots operating worldwide in 2023, a 10% annual increase, in its World Robotics 2024 report. This signals wider automation adoption, not proof that every warehouse needs an autonomous stacker. Pilot one on a representative route, record blocked trips and pallet cycle times, then compare results with manual handling. I would also check service coverage and spare-part lead times across each operating region; specifications alone can be misleading.
| Stacker Type | Typical Rated Capacity | Typical Lift Height | Aisle and Load Considerations | Automation and Operation | Best-Suited Applications | Key Selection Checks |
|---|---|---|---|---|---|---|
| Electric walkie stacker | About 1.0–2.0 tonnes | About 1.6–5.5 m, depending on mast and model | Usually suited to relatively narrow warehouse aisles; turning space depends on the truck, pallet, and load. | Powered travel and lifting; an operator walks behind and steers the truck. Not autonomous by default. | Short-distance pallet handling, low-to-medium rack storage, and smaller warehouses. | Check load weight at the required lift height, battery runtime, floor condition, and operator walking distances. |
| Electric straddle stacker | About 1.0–2.0 tonnes | About 1.6–5.5 m, depending on configuration | Outriggers straddle the load. Confirm pallet width, bottom-board design, and clearance for the support legs. | Typically operator-controlled, with powered travel and lifting; walk-behind and ride-on versions are available. | Warehouses handling a range of pallet designs where straddling support legs can fit around the load. | Verify pallet compatibility and whether the outriggers can enter the intended rack or storage location. |
| Electric counterbalanced stacker | About 1.0–2.0 tonnes | About 1.6–5.5 m, depending on configuration | Does not use front outriggers around the pallet, but generally needs adequate turning clearance and a suitable floor. | Usually operator-controlled; powered travel and lifting are common. | Handling closed-bottom pallets or loads that are awkward to approach with outrigger legs. | Compare turning radius, load centre, residual capacity at height, and clearance at rack openings. |
| Ride-on reach truck | About 1.2–2.5 tonnes | Commonly about 6–12 m; higher lifts are available on some configurations | Designed for rack aisles narrower than those typically required by counterbalanced trucks; the actual aisle depends on truck geometry and load size. | Operator-driven electric truck; automated operation requires a separate compatible automation system. | High-density pallet racking and medium-to-high lift storage in distribution and manufacturing facilities. | Check aisle width with the actual load, required lift height, mast deflection, floor flatness, and capacity at elevation. |
| Automated guided or autonomous stacker vehicle | Often about 0.5–1.5 tonnes; model-specific | Commonly designed for floor-to-low or medium-level pallet handling; confirm the specific rated lift height. | Travel paths, turning space, safety zones, and rack interfaces must be designed around the vehicle and site layout. | Uses onboard guidance and safety systems for automated transport and, where supported, pallet pickup and placement. | Repeatable pallet flows, scheduled replenishment, and operations seeking to reduce routine manual travel. | Assess pallet and rack compatibility, traffic interactions, charging strategy, safety requirements, system integration, and recovery procedures. |
| Automated storage and retrieval system (AS/RS) stacker crane | Commonly handles one pallet load per cycle; rated payload is engineered for the application. | System-specific; high-bay installations can extend to tens of metres. | Runs in a dedicated, engineered storage aisle rather than operating as a general-purpose mobile truck. | Computer-controlled crane automatically stores and retrieves loads within a rack aisle; integrated with warehouse control software. | High-volume, high-density storage with consistent unit loads and predictable inventory flows. | Evaluate throughput, rack and building design, fire protection, load tolerances, system availability, and maintenance access. |
| Figures are indicative industry ranges, not specifications for a particular model. Actual capacity, lift height, aisle requirement, and performance depend on the truck or system design, load dimensions and centre of gravity, mast, rack layout, floor conditions, and applicable local safety regulations. Confirm the manufacturer’s rated capacity and site-specific operating requirements before selection. | ||||||
Safety assessment should start with the actual warehouse, not a brochure. Measure aisle widths, floor condition, rack clearances, and the tallest planned load. During a site walkthrough, watch how people cross the stacker’s route and where blind corners occur. Check guarding, emergency stops, warning signals, and sensor coverage under realistic lighting. A sensor can miss things. Ask for documented load limits, inspection intervals, and operator training materials, then verify them with a qualified local safety professional.
Integration needs the same practical testing. Confirm that the stacker can exchange commands and status data with your warehouse software and control system. Test what happens when wireless service drops, a pallet is misidentified, or the system stops mid-task. Recovery should be clear to operators, not just an engineer. For global sites, review electrical requirements, manuals, labels, and conformity documents against the rules that apply in each destination. Requirements vary, and one certificate may not cover every market. I would still test the equipment at the receiving site; a successful factory demonstration can miss local floor markings, language needs, or workflow habits.
Choosing an automatic stacker for global warehousing means checking more than its lifting capacity. Ask suppliers for load charts, duty-cycle limits, aisle requirements, and documentation for the exact configuration you plan to use. Request a site assessment using real pallet dimensions and floor conditions. If possible, observe a comparable system operating during a busy shift. A polished demonstration is useful, but it may not reveal slowdowns around tight corners or mixed loads.
Compare the full ownership cost, not only the purchase price. Include installation, operator training, batteries or charging equipment, inspections, spare parts, and expected downtime. Ask how quickly common components can be supplied to your region, and whether support is available across your operating hours. Review warranty exclusions and service response commitments in writing. A spreadsheet can look precise while hiding assumptions. Check those assumptions with the people who maintain equipment on site. I would also revisit the shortlist after a real workflow trial; early estimates can miss awkward handoffs.
Tips: Bring several typical pallets to supplier trials. Measure travel paths, turning space, and charging access. Ask for a sample maintenance schedule and a clear escalation contact. Small details matter.
„Thanks to the LUVIR technology, the solder resist process could be switched directly from the previously used mask exposure to direct exposure. As an outstanding digital solution on the market, this technology has been able to demonstrate fast process times and superior quality on our certified conventional ink in production. This allowed us to fully digitize the solder mask process at low cost – without process or ink adjustments. An excellent benefit to our production in Rot am See.“
Ralf Göhringer (Head of Production WE Rot am See)
I would definitely recommend the Limata machine and team for a future company purchase
Michael Greenaway
Compunetics Inc.
“The Limata ldi has been amazing!! Best thing we did was buy this machine”
Richard Brady
GM
Circuitlabs
“Since 2019, we have been running the Limata X1000 LDI system (including LUVIR for solder mask imaging) in daily production as an addition to our current process with film. The machine was capable of properly exposing Taiyo PSR-4000 BN (DI) solder mask types on normal to high-copper boards using a new and unique direct imaging process. The machine operating interface is very user friendly which allowed for a quick technical training curve. The pre-registration processing reduced several seconds of production time at every print. Limata support and service staff is incomparable. They supported our team every step of the way at basically any time of the day or night, with literally, an immediate response time, customizing the software interface to best fit our Operations and needs.
We have exposed more than 8,000 prints since end of October, on various solder mask colors and some resist film panels. Limata, has proven to be very capable and innovative. They are a strong contender in the industry.
We have very much enjoyed this project, and working with the team!
Thank you Limata for the continued support and being a part of our growth.”
Bill Sezate
Vice President, GM
Summit Interconnect
As a replacement to our current contact exposure process with film, the LIMATA X2000 system including LUVIR-Technology was capable of properly exposing non-LDI solder mask types using a direct imaging process. The machine offers cutting edge software with a very intuitive operating interface which allowed for quick technician training curve. The dual drawer system combined with pre-registration processing reduced several seconds of production time at every machine cycle. Limata support and service staff is world class. They added software patches to keep production running at shortest possible response times, customized the software interface to best fit our in-house Operations system, and even wrote a step-by-step machine processing manual. As a result of the project, we have exposed more than 16,000 times on various product types and solder mask brands/colors. Limata, in a very short timeframe as a company, has definitely shown they are truly innovative and will be challenging the industry of direct imaging for the top spot.
Kevin Beattie
Process Engineer
TTM Technologies
Forest Grove Division