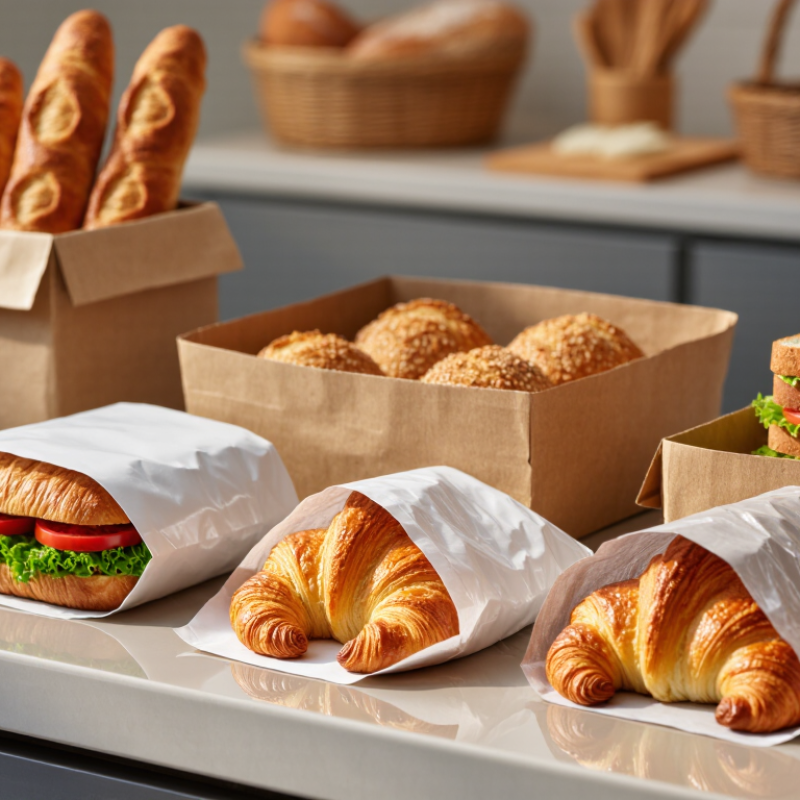
Choosing the right Food Wrapping Paper is a practical decision, not merely a branding exercise. The sheet must protect food, support safe handling, and reflect your business identity. A bakery may need grease resistance for warm pastries. A sandwich shop may require stronger paper that withstands moisture and pressure. Small details matter.
Walter Soroka, a respected packaging educator, describes packaging as “the science, art, and technology of enclosing and protecting products for distribution, storage, sale, and use.” His definition remains useful here. Food Wrapping Paper should protect the product while supporting storage, transport, presentation, and customer experience. A printed wrapper that looks attractive but leaks oil can damage trust quickly.
Start by examining the food itself. Is it hot, oily, frozen, acidic, or highly moist? Then check paper weight, coating, folding performance, grease resistance, and heat tolerance. Ask suppliers for product specifications, food-contact documentation, and clear printing details. Test the paper with your actual menu items, not only with water or empty samples. A warm croissant may expose weaknesses that a clean test cannot reveal.
There is no perfect sheet.
Cost also deserves careful thought. The cheapest option may create waste, stains, or repeated customer complaints. Yet an expensive material may offer little practical value. Recyclability claims can be confusing, especially when coatings or food residue are involved. Review supplier evidence and local disposal guidance before making promises. Your first choice may be imperfect. That is normal. Measure performance, listen to staff and customers, then improve the specification.
How to Choose Food Wrapping Paper for Your Business?
Food safety starts with intended use, not a “food-grade” label. Under FDA 21 CFR, paper components must meet applicable requirements, including 21 CFR 176.170 for aqueous or fatty foods and 21 CFR 176.180 for dry foods. Adhesives, inks, coatings, and recycled fibers need separate review. FDA 21 CFR 174.5 also expects safe use under good manufacturing practice. Record the food type, temperature, contact time, and contact area. Small details matter. Hot, oily pastries challenge paper differently than dry sandwiches. Smithers’ 2024 food-packaging analysis also identifies compliance and material performance as major purchasing considerations.
The EU approach is broader. Regulation (EC) No 1935/2004, Article 3, requires materials to avoid harmful migration and unacceptable changes in food. Article 15 covers identification and labeling. Article 16 may require a written Declaration of Compliance. Apply Regulation (EC) No 2023/2006 for good manufacturing practice. Then request migration evidence from the converter. WHO’s Estimates of the Global Burden of Foodborne Diseases reports 600 million illnesses and 420,000 deaths yearly. Wrapping paper is not the only safety control, but it is a real one. A common mistake is accepting a test report without matching its conditions to production. That assumption needs challenging. Ask for lot traceability, test methods, and worst-case scenarios. Paper may look clean. It can still transfer odor, grease, or chemicals.
Choosing food wrapping paper starts with the food, not the design. GSM means grams per square metre. It indicates basis weight, but not complete performance. A 30–40 GSM sheet suits dry pastries, cookies, and light bakery items. It folds easily and keeps portions visible. For sandwiches, use about 40–55 GSM, especially when fillings add moisture. A thin sheet can split at the corners. It happens quickly.
Greasy foods need more protection. Burgers, fried chicken, and loaded wraps often perform better with 50–70 GSM grease-resistant paper. A coated or treated surface can reduce oil transfer, but check its food-contact suitability. For hot, heavier servings, 60–90 GSM paper offers better tear resistance and handling strength. Yet thicker is not always better. It may resist folding and increase material use. I once selected a heavy grade for a delicate pastry; the package looked secure, but the customer struggled to open it.
Test paper with the actual portion, temperature, and holding time. Test it hot. Press the wrap around sharp edges and inspect the folded seams. Check wet strength after ten minutes, not just during packing. For dry snacks, 35–45 GSM may be enough; for saucy foods, move toward 60–80 GSM or use an approved barrier structure. Fit matters too. Confirm supplier specifications, migration data, and local food-contact requirements. Real service conditions can expose assumptions. Measure before ordering thousands.
Moisture and grease resistance should guide your paper selection. A paper that feels strong may still fail under a hot sandwich. In testing, Cobb60 measures water absorption over 60 seconds. The result is reported in grams per square metre. Lower values generally indicate better resistance. TAPPI T 441 is commonly used for this test. For bakery items, chilled foods, or sauces, compare results under realistic temperatures. A laboratory sample is not the whole story.
Kit ratings measure resistance to grease and oil. TAPPI T 559 uses graded chemical solutions, usually from 1 to 12. Higher ratings suggest stronger grease resistance. However, a high Kit rating does not guarantee complete protection during long contact. Folding, pinholes, printing pressure, and heat can change performance. Test the finished package, not only the paper roll.
This matters because food loss remains substantial. The FAO reports that 13.2% of food is lost between harvest and retail. The UNEP Food Waste Index Report 2024 estimates 1.05 billion tonnes of food waste in 2022. Packaging cannot solve every loss problem, but poor moisture control can worsen quality. In practical trials, place warm food inside the wrap, wait 30 minutes, and inspect the underside. Measure again after refrigeration. I would not rely on one impressive number. Real use is messier.
Choosing food wrapping paper is not only a design decision. Printing, heat sealing, and migration control can affect safety and production efficiency.
Start with the printed side. Ask whether ink can set fully before rewinding, cutting, or folding. The European Commission’s 2023 RASFF report identified chemical contamination as a recurring food-safety concern. This supports a practical rule: keep printing inks away from direct food contact whenever possible. Request ink declarations, curing records, and testing for set-off. I once saw a package pass visual inspection but fail after stacked storage. Appearance can mislead.
Heat sealing needs equal attention. Test the paper at the real machine speed, pressure, and temperature. A seal that works in a laboratory may open beside a hot filling line. Check seal strength, peel behavior, and odor after heating. Include worst-case conditions, not only the comfortable settings.
Migration testing should match the actual food. Acidic, fatty, and wet foods can extract different substances. For plastic-coated layers, EU Regulation 10/2011 sets an overall migration limit of 10 mg/dm², while specific substances may have lower limits. Paper itself is not fully harmonized across the European Union, so buyers often review national guidance, such as BfR Recommendation XXXVI. Ask for test reports using suitable simulants, contact time, and temperature. Do not accept “food grade” as complete evidence. It is too vague. Recheck the specification when ink, coating, supplier, or sealing conditions change.
How to Choose Food Wrapping Paper for Your Business?
FSC certification shows that paper comes from responsibly managed forests. However, it does not automatically mean the wrapping paper is recyclable. Ask for the certificate scope and chain-of-custody details. Also check whether coatings, inks, and adhesives affect recycling. A supplier may claim high recyclability, but local facilities might not accept the material. Request test results or written guidance for your target market. Small details matter, especially when paper touches greasy food.
Compare recyclability rates carefully. “Recyclable” is not the same as “widely recycled.” Ask how the rate was measured and under which conditions. In my purchasing reviews, uncoated paper often created fewer disposal questions. Yet it sometimes absorbed oil and required thicker material. That increased material use. The greener option was not always the thinnest one.
MOQ can change your total cost quickly. A low unit price may require thousands of sheets and expensive storage. Include printing setup, tooling, freight, inspection, damaged stock, and disposal fees. Calculate the cost per usable wrap, not per printed sheet. A simple spreadsheet helps. I once preferred a cheaper quote, then noticed its oversized cartons consumed valuable warehouse space. That decision looked efficient on paper, but it was not. Ask for a small trial order when possible. Measure wrapping speed, leakage, paper waste, and customer handling before committing to a large MOQ.
Comparison of FSC certification pathways, material-level recyclability, minimum order quantity efficiency, and relative total cost.
Uncoated paper generally offers the simplest recycling route and lowest procurement cost. Water-based coatings can improve grease resistance while preserving more recycling options than plastic or foil laminates. FSC certification applies to the responsible sourcing and traceability of fiber, while actual recycling performance depends on local collection systems and the final package structure. MOQ and cost figures are non-brand planning benchmarks and should be confirmed with supplier quotations.
Reference basis: FSC Chain of Custody principles and public paper-packaging recycling guidance. Recyclability values are indicative material-level benchmarks; MOQ efficiency is scored inversely from benchmark order quantities.
„Thanks to the LUVIR technology, the solder resist process could be switched directly from the previously used mask exposure to direct exposure. As an outstanding digital solution on the market, this technology has been able to demonstrate fast process times and superior quality on our certified conventional ink in production. This allowed us to fully digitize the solder mask process at low cost – without process or ink adjustments. An excellent benefit to our production in Rot am See.“
Ralf Göhringer (Head of Production WE Rot am See)
I would definitely recommend the Limata machine and team for a future company purchase
Michael Greenaway
Compunetics Inc.
“The Limata ldi has been amazing!! Best thing we did was buy this machine”
Richard Brady
GM
Circuitlabs
“Since 2019, we have been running the Limata X1000 LDI system (including LUVIR for solder mask imaging) in daily production as an addition to our current process with film. The machine was capable of properly exposing Taiyo PSR-4000 BN (DI) solder mask types on normal to high-copper boards using a new and unique direct imaging process. The machine operating interface is very user friendly which allowed for a quick technical training curve. The pre-registration processing reduced several seconds of production time at every print. Limata support and service staff is incomparable. They supported our team every step of the way at basically any time of the day or night, with literally, an immediate response time, customizing the software interface to best fit our Operations and needs.
We have exposed more than 8,000 prints since end of October, on various solder mask colors and some resist film panels. Limata, has proven to be very capable and innovative. They are a strong contender in the industry.
We have very much enjoyed this project, and working with the team!
Thank you Limata for the continued support and being a part of our growth.”
Bill Sezate
Vice President, GM
Summit Interconnect
As a replacement to our current contact exposure process with film, the LIMATA X2000 system including LUVIR-Technology was capable of properly exposing non-LDI solder mask types using a direct imaging process. The machine offers cutting edge software with a very intuitive operating interface which allowed for quick technician training curve. The dual drawer system combined with pre-registration processing reduced several seconds of production time at every machine cycle. Limata support and service staff is world class. They added software patches to keep production running at shortest possible response times, customized the software interface to best fit our in-house Operations system, and even wrote a step-by-step machine processing manual. As a result of the project, we have exposed more than 16,000 times on various product types and solder mask brands/colors. Limata, in a very short timeframe as a company, has definitely shown they are truly innovative and will be challenging the industry of direct imaging for the top spot.
Kevin Beattie
Process Engineer
TTM Technologies
Forest Grove Division