Global buyers are under pressure to secure reliable boards without losing control of cost, quality, or delivery time. The pcb manufacturing process now involves more than placing copper layers between fiberglass sheets. It includes material selection, impedance planning, drilling accuracy, plating control, solder-mask inspection, and final electrical testing. A small design decision can create a large purchasing problem. For example, an uncontrolled via tolerance may appear harmless in a drawing but cause signal loss during production.
Industry evidence supports a more disciplined approach. IPC’s 2024 Global Sentiment of the Electronics Industry Report highlights continuing concerns about material availability, labor capacity, lead times, and production costs. Prismark’s 2024 PCB Industry Forecast also shows how demand remains closely linked to automotive electronics, communications infrastructure, computing, and advanced digital devices. These markets require tighter process control and stronger supplier transparency. Buyers cannot judge a factory by a polished website alone. They need traceable quality records, process capability data, sample inspection results, and clear corrective-action procedures.
This guide presents ten practical tips for global purchasing teams. It connects technical details with commercial decisions, including stack-up review, design-for-manufacturing checks, testing requirements, packaging, and shipment planning. Some recommendations may seem obvious. They are still missed in real projects. No checklist eliminates every risk, especially when drawings change late or specifications remain unclear. That limitation deserves attention. Experienced buyers should question assumptions, compare evidence, and keep communication documented at every production stage. Reliable results come from repeatable processes, not optimistic promises.
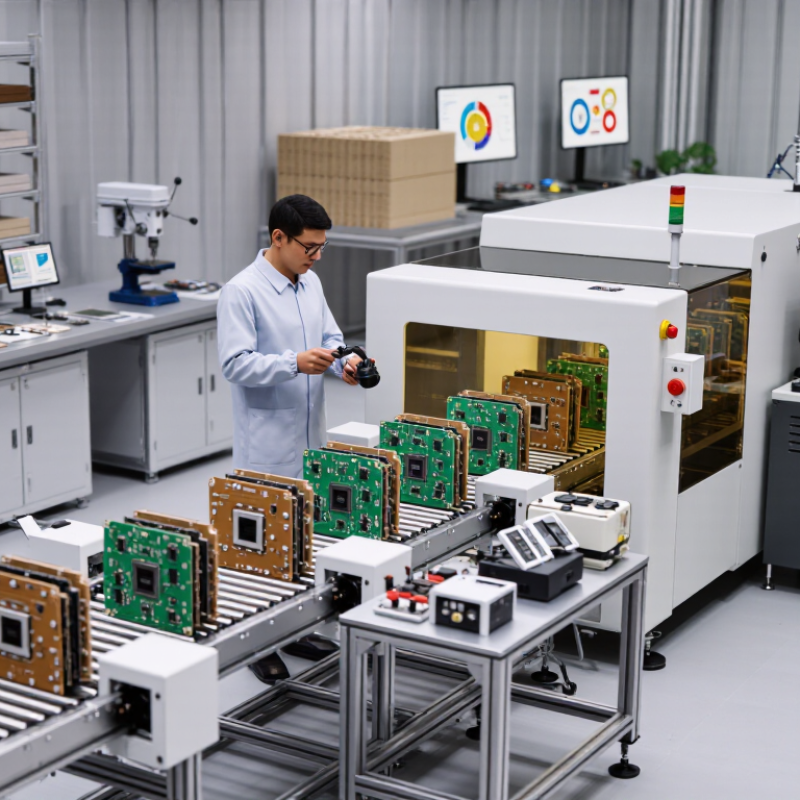
Global PCB buyers should define requirements before requesting quotations. A clear specification reduces delays, redesigns, and unexpected compliance costs. Include board dimensions, layer count, copper weight, dielectric materials, surface finish, and controlled impedance values. State the operating temperature and expected service life.
Compliance must match the destination market and the product’s use. Confirm restricted-substance requirements, material declarations, fire ratings, and applicable safety standards before production. For many projects, buyers should request evidence for RoHS, REACH, or relevant flammability requirements. Do not rely on a general “compliant” statement. Ask for test reports, certificates, revision dates, and traceable batch records.
Keep the data practical. A controlled drawing should show hole tolerances, annular rings, solder-mask clearances, and minimum spacing. The approved stack-up must match the manufactured stack-up, not only the quotation.
I have seen projects delayed because a small impedance note stayed inside an old PDF. That mistake was avoidable.
Traceability matters. Record material lot numbers, inspection results, and changes to approved files. Define who may approve substitutions or process changes. A supplier may offer a cheaper laminate, but electrical and compliance performance can shift. Check it carefully. Even experienced teams miss details when regional standards differ. Build a review step with engineering, quality, and purchasing staff before releasing the final purchase order.
Material selection shapes a PCB’s reliability before routing begins. Choose laminate based on operating temperature, signal speed, moisture exposure, and expected service life. Standard materials may reduce cost, but high-speed designs often need controlled dielectric properties. Confirm the material’s thermal expansion and glass-transition temperature with the manufacturer.
Tip 1: Define the material stack early. A small change in dielectric thickness can alter impedance, spacing, and drill design. For multilayer boards, keep power and ground planes close to signal layers. This shortens return paths and reduces unwanted noise. Copper weight also matters. Heavy copper supports higher current, yet it can complicate etching and fine-pitch fabrication.
Tip 2: Match layer structure to function, not habit. A four-layer board may suit a simple controller, while a dense communication design may require more layers. Specify finished board thickness, layer buildup, copper thickness, minimum trace width, spacing, via types, and impedance targets. One production review revealed an overlooked issue: the drawing listed nominal thickness but not tolerance. That gap caused avoidable supplier questions. Reliable specifications should include measurable limits, test methods, and acceptance criteria. Ask for stack-up confirmation before fabrication, not after prototypes arrive. Mistakes are expensive then.
Global buyers should verify a PCB manufacturer’s real capabilities before discussing price or delivery. Request a current capability sheet covering layer count, board size, copper thickness, materials, minimum trace width, spacing, and via structures. Compare these limits with your Gerber files and production volumes. Ask how the factory handles impedance control, high-density interconnects, fine-pitch components, and unusual surface finishes. Ask for evidence.
During a supplier audit, inspect the production floor rather than relying on a presentation. Check whether inspection equipment is calibrated and whether operators record results consistently. A reliable quality system should include incoming material inspection, automated optical inspection, electrical testing, final inspection, and lot-level traceability.
Review sample records, nonconformance reports, corrective actions, and process-control charts. Certificates such as ISO 9001 are useful, but confirm their scope, issuing body, and expiry date.
Do not guess.
I once treated a certificate as proof of manufacturing strength. That was a weak assumption. The supplier had a valid quality system, but its impedance testing was outsourced and poorly documented. Ask who performs each critical test, how often equipment is calibrated, and what happens when a result fails. Request recent anonymized inspection reports and a pilot run before approving mass production. Capability claims should match measurable evidence, not confident language. A factory may have excellent equipment, yet weak record discipline can still create costly variation. Review the details twice.
Global PCB buyers should treat design files as controlled production documents, not casual attachments. Use one approved archive containing schematics, Gerber files, drill data, stack-up details, and assembly drawings. Name each revision clearly, include release dates, and lock obsolete files. A missing layer or outdated drill chart can delay production for days. Keep impedance targets and material requirements visible, too.
A secure transfer method also reduces confusion. I have seen projects fail because two teams used different “final” files.
Prototypes should test more than electrical function. Check solderability, hole quality, warpage, component fit, and inspection access. Record defects with photographs and measured values. Then hold a pre-production review with engineering, purchasing, quality, and the manufacturing partner. Review yield risks, panelization, test points, packaging, and delivery assumptions.
Perfect control is unrealistic, but undocumented control is worse.
A reliable PCB order starts with controlled production information. Send the latest Gerber files, drill data, stackup, impedance targets, and approved materials in one revision package. Ask the supplier to review clearances, annular rings, copper balance, and panel utilization before fabrication. A short pilot run can reveal warpage or solder mask issues before volume production. Do not assume a perfect first build.
During production, request dated photos of inner layers, lamination, drilling, and final panels. Confirm that operators record temperature, pressure, plating thickness, and line width results. Inspection should include AOI, electrical testing, solderability checks, and microsection analysis for critical boards. Define acceptance limits in writing, including cosmetic defects and measurable tolerances. I once relied too heavily on a final inspection report. That delayed our response to a recurring plating problem.
Shipping needs the same discipline as fabrication. Use moisture-barrier packaging, desiccant, shock protection, and labels showing part number, revision, quantity, and date code. Request packing photos and verify carton counts before dispatch. Build realistic transit time into the schedule. Customs paperwork should match the commercial invoice and packing list exactly.
Keep communication simple and traceable. Assign one responsible contact on each side, then record decisions by email or a shared change log. Weekly updates should cover output, yield, defects, corrective actions, and shipment status. Ask for evidence, not vague reassurance. A rushed message can still create a costly revision mistake. Review the process after delivery, including what worked, what failed, and what should change.
„Thanks to the LUVIR technology, the solder resist process could be switched directly from the previously used mask exposure to direct exposure. As an outstanding digital solution on the market, this technology has been able to demonstrate fast process times and superior quality on our certified conventional ink in production. This allowed us to fully digitize the solder mask process at low cost – without process or ink adjustments. An excellent benefit to our production in Rot am See.“
Ralf Göhringer (Head of Production WE Rot am See)
I would definitely recommend the Limata machine and team for a future company purchase
Michael Greenaway
Compunetics Inc.
“The Limata ldi has been amazing!! Best thing we did was buy this machine”
Richard Brady
GM
Circuitlabs
“Since 2019, we have been running the Limata X1000 LDI system (including LUVIR for solder mask imaging) in daily production as an addition to our current process with film. The machine was capable of properly exposing Taiyo PSR-4000 BN (DI) solder mask types on normal to high-copper boards using a new and unique direct imaging process. The machine operating interface is very user friendly which allowed for a quick technical training curve. The pre-registration processing reduced several seconds of production time at every print. Limata support and service staff is incomparable. They supported our team every step of the way at basically any time of the day or night, with literally, an immediate response time, customizing the software interface to best fit our Operations and needs.
We have exposed more than 8,000 prints since end of October, on various solder mask colors and some resist film panels. Limata, has proven to be very capable and innovative. They are a strong contender in the industry.
We have very much enjoyed this project, and working with the team!
Thank you Limata for the continued support and being a part of our growth.”
Bill Sezate
Vice President, GM
Summit Interconnect
As a replacement to our current contact exposure process with film, the LIMATA X2000 system including LUVIR-Technology was capable of properly exposing non-LDI solder mask types using a direct imaging process. The machine offers cutting edge software with a very intuitive operating interface which allowed for quick technician training curve. The dual drawer system combined with pre-registration processing reduced several seconds of production time at every machine cycle. Limata support and service staff is world class. They added software patches to keep production running at shortest possible response times, customized the software interface to best fit our in-house Operations system, and even wrote a step-by-step machine processing manual. As a result of the project, we have exposed more than 16,000 times on various product types and solder mask brands/colors. Limata, in a very short timeframe as a company, has definitely shown they are truly innovative and will be challenging the industry of direct imaging for the top spot.
Kevin Beattie
Process Engineer
TTM Technologies
Forest Grove Division