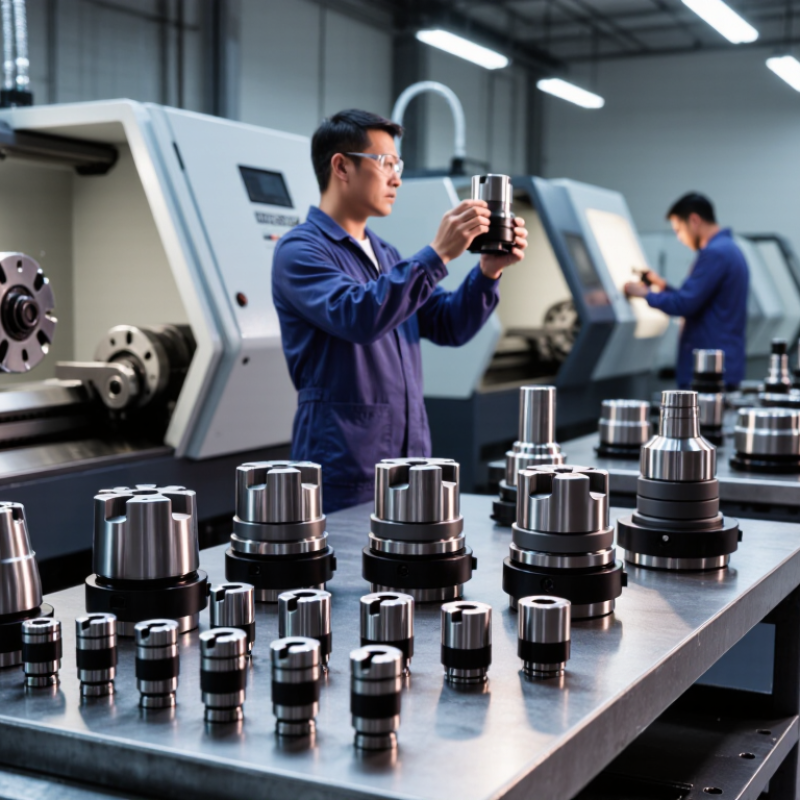
Choosing the right Turning Tool Holder is a practical decision with consequences at the cutting edge. A poor match can invite vibration, rough surfaces, and avoidable insert wear. Fit comes first. The holder must suit the lathe’s turret, the insert geometry, and the workpiece material. Then come less obvious details: shank size, clamping method, coolant access, and how far the tool must reach.
The market context is substantial, though it does not prove that any single holder design is best. Grand View Research’s Machine Tools Market Size, Share & Trends Analysis Report estimated the global machine tools market at about USD 84 billion in 2023. It projected continued growth through 2030. That scale reflects ongoing investment in machining, where repeatability and reduced downtime matter. A market forecast, however, cannot replace a trial cut on your own machine.
A sound choice starts with the actual operation: roughing, finishing, facing, or boring. Check the manufacturer’s compatibility charts, recommended cutting data, and clamping instructions. Match the holder’s rigidity and reach to the cut, rather than buying by price or appearance alone. Small details matter. A long overhang may seem convenient, yet it can reduce stability. The honest answer is that no checklist can guarantee perfect results across every setup. These seven tips will help you compare options, ask better questions, and verify the choice with measured results from your shop.
Before choosing a turning tool holder, classify the workpiece using ISO 513 material groups. Group P covers steels, while M covers stainless steels. K includes cast irons, and N covers non-ferrous metals such as aluminum. S identifies heat-resistant alloys and titanium; H covers hardened materials. These groups guide cutting-material selection, but they also help you anticipate cutting forces, heat, and chip behavior.
Check the material certificate when available. A shiny surface does not reliably identify an alloy. Stainless steel, for example, may work-harden and generate long, troublesome chips. Aluminum can demand sharp edges and generous chip space. Cast iron often produces abrasive dust, so secure clamping and suitable insert support matter. Small details count.
Match the holder’s insert seat, approach angle, and rigidity to the operation and material. A long overhang on a hardened part can invite chatter; a compact, well-supported setup is usually steadier. Still, ISO groups are broad categories, not complete machining instructions. Heat treatment, hardness, scale, and interrupted cuts can change the result. I have seen a “simple” group label hide a surprisingly difficult cut. Verify the exact grade and test a controlled pass before committing to a production setup.
A turning tool holder should match the insert code, not just its outline. ISO 1832:2017 standardizes insert designations by shape, clearance, tolerance, type, size, thickness, and nose radius. Consider CNMG 120408: “C” indicates an 80-degree rhombic shape, while “N” indicates zero clearance. In this common designation, “08” represents a 0.8 mm nose radius. Check twice. The code’s details help prevent ordering an insert that seats poorly or leaves inadequate clearance against the workpiece.
Match the holder pocket to the insert’s shape and size, then confirm the cutting direction and clearance needed for the operation. A zero-clearance insert needs a holder arrangement that provides clearance through its geometry; the insert code alone does not guarantee collision-free cutting.
The ISO designation is a useful technical reference, but always verify dimensions against the insert and holder specifications. Even experienced buyers can overlook a thickness mismatch when codes look nearly identical. A quick check with calipers can catch it.
I’d also review the intended cut: a sharp nose radius may suit lighter finishing, while a larger radius can support heavier loads but raise cutting forces. Small details matter.
Holder hand must match the direction of feed, not just the machine’s layout. On many conventional lathes, a right-hand holder cuts as the tool feeds toward the chuck; a left-hand holder suits the opposite direction. Conventions can vary, so check the holder geometry and planned tool path before mounting it. A mismatch may force awkward movement or limit access near a shoulder. A quick dry run helps.
Approach angle affects cutting forces, chip shape, and edge contact. Near a 90-degree approach angle, the cut can produce stronger radial forces, which may deflect a slender workpiece. A smaller angle shifts more force along the spindle axis and spreads the cut over a longer edge. That can help with long, flexible parts, but the wider chip needs room to escape. Watch the chip at the first pass.
For shoulder turning, choose an angle that reaches the corner without rubbing the tool body against the workpiece. Check clearance against the chuck, jaws, and nearby features, especially on short parts. I tend to focus too much on clearance at first; chip flow deserves the same attention. A setup can look right and still chatter. Test with a light cut, inspect the surface, and adjust the holder or feed direction if the sound or finish changes.
A turning tool holder can look correct and still sit poorly in the turret. Check its ISO 5608 designation against the holder drawing and the machine’s requirements. The code identifies key features, but do not rely on memory or a partial match. Confirm the shank height, width, and overall length in millimetres. A small height mismatch can shift the cutting edge from the spindle centreline.
Check the holder style, insert shape, clearance angle, and hand of cut as well. These details affect insert fit and cutting direction. Compare the designation with the insert specification and the actual seat, especially when replacing an older holder. Look for clear, undamaged locating surfaces; chips or burrs can prevent the holder from seating flat. It happens. I have seen a nominally matching tool create setup trouble because one dimension was overlooked. Check the current standard or a reliable technical drawing when codes seem ambiguous. A quick measurement with a caliper helps, but it cannot confirm every geometric feature. Verify the full designation before ordering or setting up the tool.
Tool overhang is easy to underestimate: an extra few millimeters can turn a clean cut into chatter. For a cantilevered tool, deflection rises with the cube of unsupported length. A 20% increase in overhang therefore creates about 73% more deflection under the same load and tool geometry. This follows the standard beam equation, δ = FL³/(3EI), used in engineering mechanics and machining-dynamics analysis. Keep the holder close to the work, and choose the shortest projection that clears the chuck and shoulder. Small change, big effect.
Coolant delivery matters just as much. Aim the nozzle at the cutting edge, not merely at the general cutting zone; verify flow with the tool installed and the turret in its working position. A stream that hits the chip may miss the tool–workpiece interface. Check for blocked passages, leaks, and chip buildup, then match coolant pressure and flow to the holder’s design and the machine’s limits. ISO 3685:1993 provides repeatable tool-life test conditions for single-point turning, helping shops compare wear instead of relying on surface finish alone. I still recheck alignment after a tool change.
Record overhang, coolant setup, and wear for each trial. That simple log makes troubleshooting more reliable, though it will not explain every vibration. Schmitz and Smith’s Machining Dynamics (2nd edition, 2019) discusses how tool-system dynamics affect stability; in practice, even a sound setup can behave differently as the workpiece gets longer or thinner.
„Thanks to the LUVIR technology, the solder resist process could be switched directly from the previously used mask exposure to direct exposure. As an outstanding digital solution on the market, this technology has been able to demonstrate fast process times and superior quality on our certified conventional ink in production. This allowed us to fully digitize the solder mask process at low cost – without process or ink adjustments. An excellent benefit to our production in Rot am See.“
Ralf Göhringer (Head of Production WE Rot am See)
I would definitely recommend the Limata machine and team for a future company purchase
Michael Greenaway
Compunetics Inc.
“The Limata ldi has been amazing!! Best thing we did was buy this machine”
Richard Brady
GM
Circuitlabs
“Since 2019, we have been running the Limata X1000 LDI system (including LUVIR for solder mask imaging) in daily production as an addition to our current process with film. The machine was capable of properly exposing Taiyo PSR-4000 BN (DI) solder mask types on normal to high-copper boards using a new and unique direct imaging process. The machine operating interface is very user friendly which allowed for a quick technical training curve. The pre-registration processing reduced several seconds of production time at every print. Limata support and service staff is incomparable. They supported our team every step of the way at basically any time of the day or night, with literally, an immediate response time, customizing the software interface to best fit our Operations and needs.
We have exposed more than 8,000 prints since end of October, on various solder mask colors and some resist film panels. Limata, has proven to be very capable and innovative. They are a strong contender in the industry.
We have very much enjoyed this project, and working with the team!
Thank you Limata for the continued support and being a part of our growth.”
Bill Sezate
Vice President, GM
Summit Interconnect
As a replacement to our current contact exposure process with film, the LIMATA X2000 system including LUVIR-Technology was capable of properly exposing non-LDI solder mask types using a direct imaging process. The machine offers cutting edge software with a very intuitive operating interface which allowed for quick technician training curve. The dual drawer system combined with pre-registration processing reduced several seconds of production time at every machine cycle. Limata support and service staff is world class. They added software patches to keep production running at shortest possible response times, customized the software interface to best fit our in-house Operations system, and even wrote a step-by-step machine processing manual. As a result of the project, we have exposed more than 16,000 times on various product types and solder mask brands/colors. Limata, in a very short timeframe as a company, has definitely shown they are truly innovative and will be challenging the industry of direct imaging for the top spot.
Kevin Beattie
Process Engineer
TTM Technologies
Forest Grove Division
