Choosing among China’s top 10 Astm A106 Pipe manufacturers requires more than comparing prices. ASTM A106 Pipe is commonly selected for high-temperature service, steam lines, process piping, and refinery applications. Yet, not every supplier offers the same manufacturing control. Differences appear in steel chemistry, heat treatment, wall-thickness consistency, and documentation quality.
A practical evaluation should begin with the mill’s production experience. Can it provide recent heat numbers and complete material test certificates? Does its laboratory verify tensile strength, yield strength, elongation, and hydrostatic performance? These details matter when pipes face pressure, heat, and repeated thermal cycling. Small differences can become expensive failures.
Metallurgy author John D. Verhoeven wrote, “The properties of a material are determined by its structure.” This principle applies directly to ASTM A106 Pipe. Chemical composition alone does not guarantee dependable service. Rolling practice, normalizing treatment, inspection discipline, and storage conditions also influence performance. A serious manufacturer should explain these controls clearly.
Factory visits can reveal practical evidence. Look for marked pipe bundles, protected bevels, calibrated gauges, and traceable inspection records. Ask for references from projects using comparable sizes and schedules. Be cautious with impressive websites. They are not proof.
This comparison will examine ten leading Chinese manufacturers through product range, certifications, export experience, testing capacity, and customer support. Rankings remain imperfect. A supplier suitable for a small boiler project may not fit a critical petrochemical line. Buyers should verify every claim against current documents, applicable specifications, and independent inspection requirements.
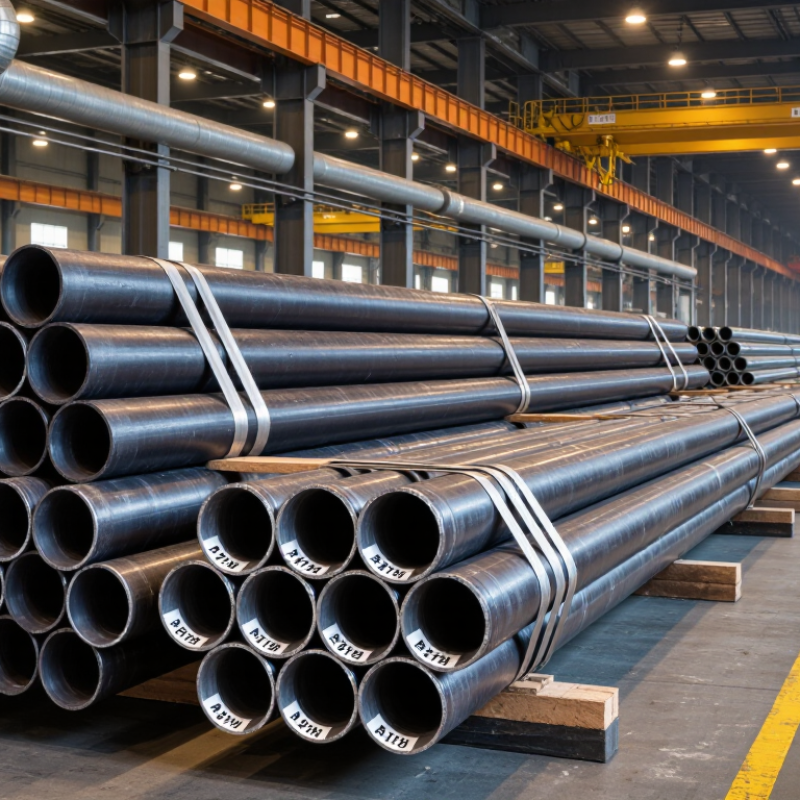
ASTM A106 pipe is a seamless carbon steel pipe designed for high-temperature service. It is commonly supplied in Grades A, B, and C. Grade B is often selected for balanced strength, weldability, and cost. The standard controls chemical composition, tensile properties, dimensions, and testing requirements. Its seamless construction removes a longitudinal weld seam. That matters in demanding pressure systems.
ASTM A106 pipe is widely used because it performs reliably in hot process environments. Refineries, power stations, chemical plants, and boiler systems commonly specify it. A pipe rack may carry steam near 400°C, while process lines handle oil, gas, or water. Engineers value its predictable fabrication behavior and broad availability. Welders can prepare, join, and inspect it using established procedures. However, service temperature, pressure, wall thickness, and corrosion allowance must match the design.
A common mistake is treating A106 as a universal pipe solution. It is not automatically corrosion-resistant or suitable for every fluid. Engineers must verify mill certificates, heat numbers, hydrostatic tests, and non-destructive examination records. Small details can expose weak quality control. Specifications are sometimes read too quickly. That oversight can lead to incorrect grade selection, premature thinning, or unsafe installation. Careful manufacturer evaluation remains essential, especially when production consistency matters.
China Top 10 ASTM A106 Pipe Manufacturers?
How China’s Top ASTM A106 Pipe Manufacturers Are Selected
Selecting leading ASTM A106 pipe manufacturers requires more than checking production capacity. A reliable review examines material traceability, furnace records, heat numbers, and inspection procedures. Manufacturers should provide valid certificates for chemical composition, tensile strength, yield strength, and hydrostatic testing. Their pipes should match the required Grade A, B, or C specification. Factory experience also matters, especially for high-temperature service and pressure pipeline projects.
Independent audits can reveal practical details that brochures often miss. Inspectors may review calibration records, welding controls, ultrasonic testing, and surface-finish consistency. Delivery performance deserves attention too. A technically strong supplier can still create problems through weak packaging or incomplete documents. We also consider export experience, technical communication, and after-sales handling. No ranking is perfect. Buyer requirements differ, and published information may change.
Tips: Request recent mill test certificates and sample inspection reports. Confirm dimensions, wall thickness, end preparation, and coating requirements before ordering. Visit the facility when possible, or use an independent inspection agency. Ask how rejected pipes are identified and isolated. Small details matter. A clear sampling plan can prevent costly misunderstandings. Excellent claims should still be checked against physical evidence.
Mechanical performance is one of the key technical benchmarks used when evaluating ASTM A106 seamless carbon steel pipe manufacturers. The chart compares the ASTM A106/A106M minimum tensile and yield strength requirements for Grades A, B, and C.
Selection insight: Manufacturers should provide traceable mill test certificates demonstrating that supplied pipes meet or exceed the specified ASTM A106 grade requirements. Higher-strength grades require stronger tensile and yield performance.
China’s top 10 ASTM A106 pipe manufacturers are best judged by evidence, not production claims. ASTM A106 covers seamless carbon steel pipe for high-temperature service, with Grade B widely specified for process lines. Buyers should verify heat numbers, mill certificates, tensile results, and hydrostatic testing. A polished website is not enough.
The World Steel Association reported that China produced about 1.02 billion tonnes of crude steel in 2023. This scale supports strong tube-making capacity, yet capacity does not guarantee consistent pipe quality. The International Trade Centre’s trade data also shows China remains a major global exporter of iron and steel products. For the top ten manufacturers, practical screening should include API-style quality systems, EN 10204 3.1 documentation, third-party inspection access, and proven export packaging.
Details matter. Ask whether each mill controls piercing, heat treatment, straightening, and ultrasonic inspection internally. Check whether pipe ends arrive beveled, capped, and marked for traceability. Grand View Research identifies energy and industrial infrastructure as major drivers of seamless pipe demand, but market forecasts are not purchase guarantees. A ranking may also hide weaknesses. Some suppliers excel in large diameters, while others perform better with small-bore schedules. Test reports can look complete, but sampling limits still deserve attention. Confirm current mill capacity, delivery records, and nonconformance handling before treating any “top 10” list as final.
Comparing China’s leading ASTM A106 pipe manufacturers requires more than production figures. Quality starts with steel chemistry, heat treatment, and traceable testing. Serious producers provide heat numbers, dimensional records, and hydrostatic test results for each batch. Their laboratories check tensile strength, yield strength, elongation, and bend performance against project requirements. A polished certificate is not enough. I would also inspect sampling methods and calibration dates. Small gaps here can become costly field problems.
Capacity separates a stable supplier from a crowded workshop. Larger facilities may operate multiple seamless piercing lines, furnaces, and finishing bays. This matters when a project needs several diameters, schedules, and delivery lots. Yet installed capacity can mislead. Ask for recent monthly output, normal utilization, and available heat-treatment slots. A factory producing 20,000 tonnes annually may still struggle with urgent small orders. In my experience, planning discipline often matters more than a large headline number. Still, capacity claims deserve independent verification.
The strongest manufacturers balance consistency with practical responsiveness. They should explain how nonconforming pipes are isolated, replaced, and documented. Packaging also reveals experience: capped ends, moisture protection, and clear bundle markings reduce transport damage. Lead time should include inspection, packing, and port handling, not only mill production. Some suppliers communicate well before signing, then become vague after payment. That warning deserves attention. A fair comparison should weigh defect rates, repeat-order performance, audit findings, and technical support alongside price. No ranking is permanent; equipment upgrades and management changes can quickly alter the picture.
Choosing an ASTM A106 pipe manufacturer requires more than comparing prices. Confirm that the factory understands seamless carbon steel pipe production and the required service temperature. Ask for recent mill test certificates, chemical analysis, tensile results, and hydrostatic test records. Documents should match the actual heat number on each pipe.
Production experience matters. A reliable manufacturer can explain wall thickness control, heat treatment, ultrasonic testing, and dimensional inspection in clear terms. Request photos of marking, packing, and loading procedures. Better still, arrange an independent inspection before shipment. Small details matter, such as clean pipe ends, accurate bevels, and dry internal surfaces.
Check traceability from raw material to final delivery. The supplier should provide a quality plan, inspection records, and a realistic delivery schedule. Do not trust a polished website alone. I have seen impressive claims weakened by missing test data.
That is a warning sign.
Communication also reveals technical strength. Ask how the manufacturer handles nonconforming pipes, replacement requests, and coating or packaging changes. Their answer should be specific, not merely reassuring.
A low quotation can hide weak inspection or costly delays. Sometimes, the cheapest option is not economical. Review production capacity, export experience, payment protection, and after-sales response together. Leave room for doubt, and verify every important claim.
„Thanks to the LUVIR technology, the solder resist process could be switched directly from the previously used mask exposure to direct exposure. As an outstanding digital solution on the market, this technology has been able to demonstrate fast process times and superior quality on our certified conventional ink in production. This allowed us to fully digitize the solder mask process at low cost – without process or ink adjustments. An excellent benefit to our production in Rot am See.“
Ralf Göhringer (Head of Production WE Rot am See)
I would definitely recommend the Limata machine and team for a future company purchase
Michael Greenaway
Compunetics Inc.
“The Limata ldi has been amazing!! Best thing we did was buy this machine”
Richard Brady
GM
Circuitlabs
“Since 2019, we have been running the Limata X1000 LDI system (including LUVIR for solder mask imaging) in daily production as an addition to our current process with film. The machine was capable of properly exposing Taiyo PSR-4000 BN (DI) solder mask types on normal to high-copper boards using a new and unique direct imaging process. The machine operating interface is very user friendly which allowed for a quick technical training curve. The pre-registration processing reduced several seconds of production time at every print. Limata support and service staff is incomparable. They supported our team every step of the way at basically any time of the day or night, with literally, an immediate response time, customizing the software interface to best fit our Operations and needs.
We have exposed more than 8,000 prints since end of October, on various solder mask colors and some resist film panels. Limata, has proven to be very capable and innovative. They are a strong contender in the industry.
We have very much enjoyed this project, and working with the team!
Thank you Limata for the continued support and being a part of our growth.”
Bill Sezate
Vice President, GM
Summit Interconnect
As a replacement to our current contact exposure process with film, the LIMATA X2000 system including LUVIR-Technology was capable of properly exposing non-LDI solder mask types using a direct imaging process. The machine offers cutting edge software with a very intuitive operating interface which allowed for quick technician training curve. The dual drawer system combined with pre-registration processing reduced several seconds of production time at every machine cycle. Limata support and service staff is world class. They added software patches to keep production running at shortest possible response times, customized the software interface to best fit our in-house Operations system, and even wrote a step-by-step machine processing manual. As a result of the project, we have exposed more than 16,000 times on various product types and solder mask brands/colors. Limata, in a very short timeframe as a company, has definitely shown they are truly innovative and will be challenging the industry of direct imaging for the top spot.
Kevin Beattie
Process Engineer
TTM Technologies
Forest Grove Division