Hydrophobic Vent components protect sealed products from water, dust, and pressure changes while allowing air to pass through. A microporous membrane can help prevent liquid entry, but performance depends on pore structure, housing design, and exposure conditions. A vent that works well in a dry sensor enclosure may not suit a device exposed to oils, cleaning fluids, or repeated temperature swings. Details matter.
This 2026 supplier overview looks beyond product names. It considers documented performance data, material options, quality controls, customization, technical support, and practical availability. Buyers can compare solutions for outdoor electronics, lighting, sensors, and battery enclosures, where trapped moisture or pressure buildup can affect reliability. Small gaps matter. So do mounting methods and the enclosure’s surface.
No supplier fits every design. A published water-entry rating is useful, yet it does not replace testing in the finished product. Ask how samples were tested, which fluids were involved, and whether results reflect your operating temperature and pressure range. Those questions can reveal differences hidden by similar datasheets. This guide is intended to help engineers and purchasing teams make a clearer shortlist, not to declare one universal winner. Some comparisons will remain imperfect, because supplier data and real-world conditions do not always line up neatly. That uncertainty deserves attention, not gloss.
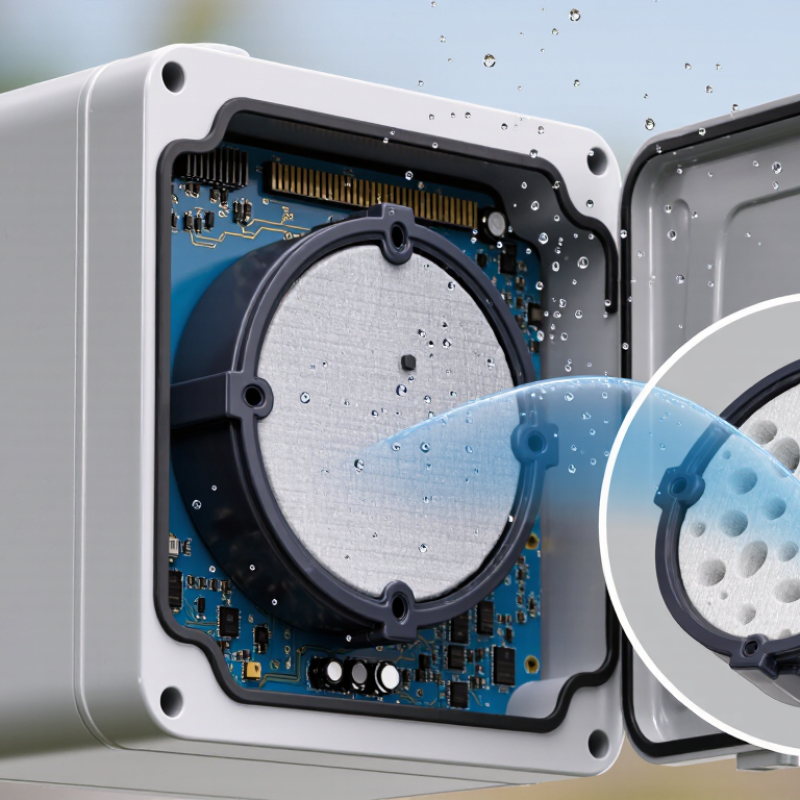
A hydrophobic vent uses a microporous membrane to let air pass while resisting liquid water. Its pores are small enough to create a barrier: water must overcome surface tension before entering them. Because the membrane repels water, droplets bead on its surface rather than readily soaking through. Air still moves through the connected pores, helping equalize pressure inside an enclosure.
The details matter. A vent exposed to splashes may perform differently from one submerged under pressure. Detergents, oils, or other contaminants can reduce water repellency, and excessive pressure may force water through. Not magic. Engineers therefore consider pore structure, membrane area, airflow needs, and the enclosure’s exposure conditions together. A vent that is too small can slow pressure equalization; a poorly placed one may collect water around its edges. In practical testing, check the assembled product, not just a membrane sample. Seals and mounting surfaces can become weak points. Ratings are useful, but real use can be messier than a clean test setup.
Top Hydrophobic Vent Suppliers in 2026
For hydrophobic vent selection, an IPX7 claim needs careful reading. Under IEC 60529, IPX7 testing means temporary immersion in water, typically at a depth of 1 metre for 30 minutes. It does not mean protection at any depth or for unlimited time. The exact test conditions and product configuration matter. Small detail, big difference.
A vent’s performance also depends on its membrane, housing, seals, and installation. A hydrophobic membrane can help resist liquid water while allowing air to pass, but a poorly seated gasket may create a leak path. Ask suppliers for test reports showing what assembly was tested, how it was mounted, and whether the result applies to your intended design. IPX7 does not automatically demonstrate resistance to powerful water jets; that requires separate assessment. Real-world performance may vary, and that part is easy to overlook.
Tips: Confirm the 1-metre, 30-minute test scope. Check the seal compression and vent orientation in your own enclosure. If the product will face spray as well as immersion, request relevant test evidence rather than relying on an IPX7 label alone.
Use these criteria to compare suppliers. Airflow, water-entry pressure, and environmental limits are product-specific; request test reports for the exact vent and installation rather than assuming universal pass values.
| Evaluation dimension | Benchmark or requirement | Evidence to request from supplier | Why it matters |
|---|---|---|---|
| Water ingress protection | IPX7 under IEC 60529 is a temporary-immersion test commonly summarized as immersion in water at 1 m for 30 minutes. Confirm the applicable standard conditions and tested assembly. | Test report identifying the vent, enclosure, mounting method, orientation, and test conditions. | An IPX7 claim applies to the tested enclosure configuration; it does not automatically establish the rating of every installation. |
| Continuous immersion claim | IPX7 alone does not specify continuous immersion. IPX8 conditions are agreed between the manufacturer and user and should state depth and duration. | Written IPX8 test conditions and supporting test documentation, if continuous immersion is required. | Prevents treating a temporary-immersion result as proof of suitability for prolonged submersion. |
| Airflow / pressure equalization | Set the required airflow at a stated differential pressure for the application; there is no single universal airflow benchmark for hydrophobic vents. | Airflow-versus-pressure data, test method, sample configuration, and any stated tolerance. | Adequate venting can help reduce pressure differentials while preserving the specified barrier function. |
| Water-entry pressure | Specify a project-specific minimum and test conditions; results depend on the membrane, construction, and test method. | Water-entry-pressure test report with units, method, sample details, and acceptance criteria. | Provides a measurable comparison of resistance to liquid-water penetration under defined conditions. |
| Ingress protection of the installed vent | Evaluate the complete assembly, including vent, housing, seal, cutout, and fastening method, against the required enclosure rating. | Installation instructions and test evidence for the relevant assembly, not only membrane material data. | Installation details can affect sealing and the resulting enclosure performance. |
| Temperature and chemical compatibility | Match the specified operating-temperature range and exposure conditions to the product and application; limits vary by construction. | Product datasheet plus compatibility or aging-test data for relevant fluids, cleaning agents, and temperature cycles. | Heat, chemicals, and aging may affect membrane, housing, or adhesive performance. |
| Mounting and sealing options | Select a mounting format compatible with the enclosure design, such as adhesive-backed, threaded, or press-fit, where offered. | Dimensional drawings, recommended cutout, assembly guidance, and seal details. | Fit and installation repeatability are important to achieving the intended enclosure protection. |
| Traceability and quality documentation | Require lot identification and documented inspection or test controls appropriate to the application. | Sample certificate, lot-traceability details, and quality-system documentation relevant to the order. | Supports incoming inspection, change control, and investigation of field issues. |
Selection note: Compare suppliers using the same test methods, mounting configuration, and acceptance criteria. An IPX7 test result should not be interpreted as a guarantee of continuous immersion performance.
For a hydrophobic vent, a pore-size number means little without a clear test method. ASTM F316 evaluates membrane pore characteristics using bubble-point and mean-flow-pore procedures. The sample must be fully wetted with a suitable low-surface-tension liquid; water may not enter hydrophobic pores reliably. That detail matters. Ask suppliers to state the wetting fluid, temperature, test area, and pressure ramp used.
During a bubble-point test, pressure rises until gas passes through the largest wetted pore. The first steady stream is the key observation, not a few stray bubbles at the edge. A mean-flow test compares gas flow through a wetted sample with flow through the dry sample, helping describe the pore distribution. Results depend on setup and handling. A folded coupon or incomplete wetting can mislead.
When comparing suppliers in 2026, request actual test records, sample identification, and acceptance limits—not only a catalog value. Check whether the tested membrane matches the production lot and finished vent construction. ASTM F316 characterizes pore structure; it does not by itself confirm airflow, water-entry pressure, or service life in an assembly. A supplier’s report should make those limits plain. Some reports still leave questions. Ask them.
When comparing hydrophobic vent suppliers, start with material and use conditions, not catalog labels. Expanded PTFE is common where airflow and water resistance matter; polypropylene and polyethylene may suit different cost, chemical, or assembly needs. No material wins every test. Check the actual fluid, temperature range, and exposure duration.
Formats change installation and serviceability. Adhesive-backed vents fit flat housings, while press-fit or threaded designs can offer more secure mechanical retention. Compare airflow, water-entry pressure, pore structure, and sealing method using test data for the finished vent. A membrane alone does not guarantee housing performance.
Grand View Research valued the global membrane filtration market at USD 17.71 billion in 2023 and forecast an 8.1% CAGR through 2030. This broad market figure is not a hydrophobic-vent forecast, but it signals growing attention to membrane-based products.
Ask suppliers for test methods and results, plus sample parts for assembly trials.
A spec sheet can look reassuring. Real housings sometimes disagree. That detail is easy to overlook.
When comparing hydrophobic vent suppliers in 2026, start with the enclosure, not the catalogue. Estimate the pressure changes caused by heating, cooling, altitude, and rapid temperature swings. Then check whether the vent’s airflow capacity can equalize pressure quickly enough for your device. A small electronics enclosure near a warm motor may need different performance from a sealed outdoor sensor. Ask suppliers for airflow data at a stated pressure differential, not just a headline value. Details matter.
Water entry pressure and IP requirements answer related, but different, questions. Water entry pressure describes the pressure at which water may penetrate the vent under specified test conditions. An IP rating applies to a tested enclosure configuration, so a component’s rating alone does not certify the finished product. Request test methods, sample details, and limits such as water temperature or exposure time. Check the actual assembly, too: a poorly seated gasket can undermine a capable membrane. It happens.
Compare results against the real installation. A vent exposed to spray, dust, detergent, or repeated washing may need different validation than one inside a sheltered housing. Confirm operating temperature, chemical compatibility, membrane area, adhesive options, and mounting tolerances. Suppliers should explain how their data applies to your geometry and offer samples for enclosure-level trials. If a specification feels vague, pause and ask for the conditions behind it. That extra check can prevent a costly redesign.
„Thanks to the LUVIR technology, the solder resist process could be switched directly from the previously used mask exposure to direct exposure. As an outstanding digital solution on the market, this technology has been able to demonstrate fast process times and superior quality on our certified conventional ink in production. This allowed us to fully digitize the solder mask process at low cost – without process or ink adjustments. An excellent benefit to our production in Rot am See.“
Ralf Göhringer (Head of Production WE Rot am See)
I would definitely recommend the Limata machine and team for a future company purchase
Michael Greenaway
Compunetics Inc.
“The Limata ldi has been amazing!! Best thing we did was buy this machine”
Richard Brady
GM
Circuitlabs
“Since 2019, we have been running the Limata X1000 LDI system (including LUVIR for solder mask imaging) in daily production as an addition to our current process with film. The machine was capable of properly exposing Taiyo PSR-4000 BN (DI) solder mask types on normal to high-copper boards using a new and unique direct imaging process. The machine operating interface is very user friendly which allowed for a quick technical training curve. The pre-registration processing reduced several seconds of production time at every print. Limata support and service staff is incomparable. They supported our team every step of the way at basically any time of the day or night, with literally, an immediate response time, customizing the software interface to best fit our Operations and needs.
We have exposed more than 8,000 prints since end of October, on various solder mask colors and some resist film panels. Limata, has proven to be very capable and innovative. They are a strong contender in the industry.
We have very much enjoyed this project, and working with the team!
Thank you Limata for the continued support and being a part of our growth.”
Bill Sezate
Vice President, GM
Summit Interconnect
As a replacement to our current contact exposure process with film, the LIMATA X2000 system including LUVIR-Technology was capable of properly exposing non-LDI solder mask types using a direct imaging process. The machine offers cutting edge software with a very intuitive operating interface which allowed for quick technician training curve. The dual drawer system combined with pre-registration processing reduced several seconds of production time at every machine cycle. Limata support and service staff is world class. They added software patches to keep production running at shortest possible response times, customized the software interface to best fit our in-house Operations system, and even wrote a step-by-step machine processing manual. As a result of the project, we have exposed more than 16,000 times on various product types and solder mask brands/colors. Limata, in a very short timeframe as a company, has definitely shown they are truly innovative and will be challenging the industry of direct imaging for the top spot.
Kevin Beattie
Process Engineer
TTM Technologies
Forest Grove Division