A flooded basement is not a controlled test bay. Mud, leaves, narrow pits, and changing water levels can expose a pump’s limits quickly. Choosing a Submersible Drainage Pump therefore means looking beyond horsepower. Flow at the required head, solids passage, float-switch behavior, and discharge-hose size all matter.
The U.S. Department of Energy’s Improving Pumping System Performance sourcebook reports that pumping systems account for nearly 20% of global electricity demand. That figure covers pumping systems broadly, not drainage pumps alone, but it shows why efficient matching matters. A pump that runs outside its useful operating range may waste energy and wear sooner. In Johann Friedrich Gülich’s pump-engineering approach, selection centers on the real duty point; paraphrased: “Choose for the system’s actual flow and head, not the nameplate alone.” His book, Centrifugal Pumps, is a technical reference for pump design and operation.
This guide compares ten leading drainage-pump options by capacity, solids handling, construction, controls, and practical service needs. We also distinguish clean-water duties from dirty-water jobs, where a small intake screen can clog fast. Details matter. Ratings can be confusing, and published performance may not match a long hose or a deep lift. That deserves a second look. The right choice depends on the site, not just the product ranking.
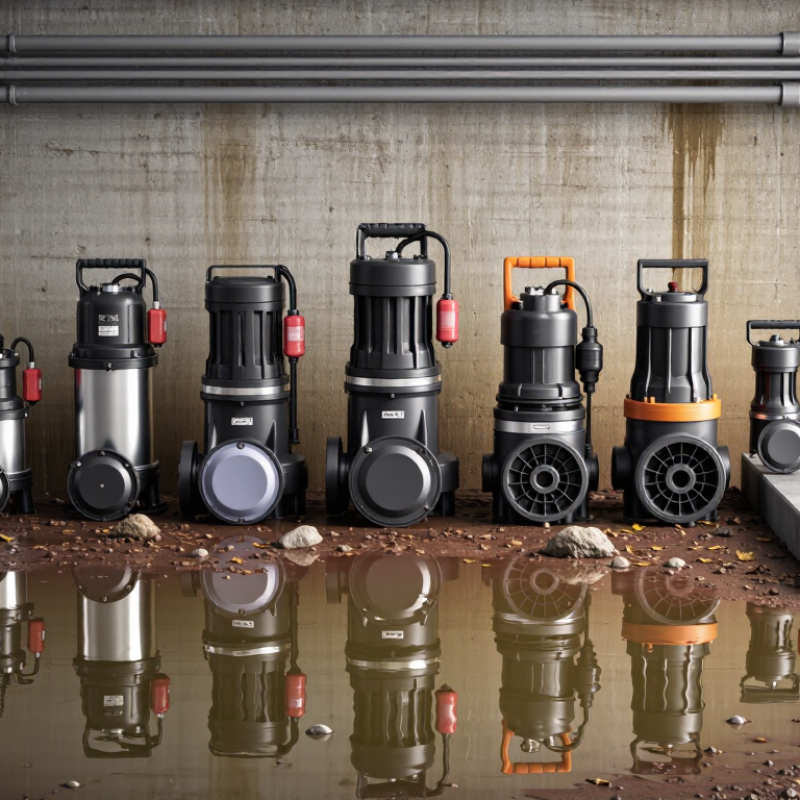
A submersible drainage pump sits directly in the water it moves. Inside its sealed housing, an electric motor spins an impeller. The impeller draws water through an intake screen and pushes it into a discharge hose or pipe. The hose carries water away from a basement, window well, or shallow work area. The pump must stay submerged as specified by its manufacturer.
Many pumps use a float switch to control operation. As water rises, the float lifts and starts the motor. When the water level falls, the float drops and switches the pump off. Simple, but not foolproof. A float can snag against a wall or hose, so leave it room to move. Some models use electronic sensors instead.
Performance depends on more than motor power. The pump’s lift height, hose length, and bends all affect how quickly water flows. Less lift usually means easier flow. Check the intake for leaves, grit, or small stones; not every drainage pump can handle muddy water. In practice, placing the pump on a flat brick or firm base can keep it from sucking up sediment. Avoid running it dry, and follow the manual’s instructions for electrical connections and minimum water depth.
When comparing the 10 best submersible drainage pumps, start with flow rate and total dynamic head. The pump must move water at the required height, not just match a headline flow figure. Check the performance curve at your actual discharge height. A basement pit and a muddy construction trench need different capacities.
Solids handling matters. Compare the permitted particle size with the likely debris, such as grit or small leaves. Check casing material, seal design, thermal protection, and whether the pump supports continuous or intermittent operation. The U.S. Department of Energy’s 2006 Improving Pumping System Performance sourcebook reports that pumping systems use nearly 20% of global electricity. That figure covers pumping systems broadly, but it underscores why efficiency deserves attention. Not just motor power. Compare energy use at the operating point, and consider how easily the unit can be inspected and serviced. A caveat: published test conditions may not match a real site. Verify head, flow, and solids limits against the manufacturer’s curve and installation instructions before choosing.
Ten noteworthy submersible drainage pump choices include compact clean-water pumps, dirty-water pumps, solids-handling pumps, automatic float-switch pumps, vertical-float pumps, low-level drainage pumps, high-head pumps, stainless-steel pumps, cast-iron pumps, and portable battery-backup pumps. Each suits a different job. Clean-water units can handle a flooded utility room, while solids-handling designs are better for water containing grit or debris. High-head pumps can lift water farther, though their flow usually drops as discharge height increases.
A pump’s advertised flow rate can look persuasive, but it may describe performance under ideal conditions. Check the required lift, hose diameter, water clarity, and permitted particle size before choosing. A float switch needs room to move freely; a cramped sump can stop it from starting. I would not select a pump by material alone, either. Tough construction matters, but correct sizing matters more.
Tips: Keep the pump upright and never lift it by its power cable. Clear debris from the intake, test the float, and avoid running the unit dry. Use a properly protected power supply, and follow the manual’s instructions for wet locations. Small details matter.
When comparing ten leading submersible drainage pumps, rated flow alone can mislead. A pump may advertise a high flow rate but move much less water through a long hose or up several metres. Check its performance curve at your expected lift, and account for hose bends and friction. For a flooded basement, dependable flow under real conditions matters more than an impressive headline figure. Small details count.
Solids handling is equally important. A pump designed for relatively clear water may struggle with leaves, grit, or small debris. Check the manufacturer’s stated particle size and whether the intake can clog easily. A wide intake can help, but it does not make every pump suitable for muddy water. There is a trade-off. Larger solids capacity can come with different flow performance, so compare both specifications rather than guessing from appearance.
Durability depends on more than a tough-looking casing. Look for corrosion-resistant materials, a well-protected motor, and a mechanical seal suited to repeated immersion. A float switch should move freely, without catching on a pit wall or hose. Maintenance still matters: rinse sediment from the intake and inspect the cable and seals regularly. No pump is perfect; a small overlooked blockage can undo an otherwise sensible choice.
Drainage needs differ more than pump labels suggest. A basement seepage pit needs steady, automatic removal, while a construction trench may contain grit and larger debris. Match the pump’s flow rate to the required lift and discharge distance; rated flow often drops as the water rises. Check the pump curve. Also verify the solids-passage size, float-switch range, and whether the unit can handle continuous operation.
A useful first estimate comes from the U.S. Geological Survey: one inch of rain on one acre produces about 27,154 gallons of water. That figure is not a pump-sizing result, since runoff, soil, and collection area change the actual load. Still, it shows why a broad, shallow yard can overwhelm a small sump during a storm. NOAA Atlas 14 precipitation-frequency data can help compare local rainfall intensities when planning drainage capacity.
For muddy water, choose a model rated for suspended solids, and keep its intake clear of fabric or leaves. For a narrow sump, measure the pit before choosing a pump; a wide float may jam against the wall. A high-head pump suits a long uphill discharge, but it may move less water than expected. Check the operating curve at the actual lift, not just the maximum-flow figure. It’s easy to overlook backflow, too. A check valve and accessible power connection make maintenance simpler, though site conditions can still defeat a neat calculation.
This chart compares representative maximum particle sizes that different drainage pump types may handle. Actual capacities vary by model; check the manufacturer’s specifications, and match the pump to the required flow rate and discharge head.
„Thanks to the LUVIR technology, the solder resist process could be switched directly from the previously used mask exposure to direct exposure. As an outstanding digital solution on the market, this technology has been able to demonstrate fast process times and superior quality on our certified conventional ink in production. This allowed us to fully digitize the solder mask process at low cost – without process or ink adjustments. An excellent benefit to our production in Rot am See.“
Ralf Göhringer (Head of Production WE Rot am See)
I would definitely recommend the Limata machine and team for a future company purchase
Michael Greenaway
Compunetics Inc.
“The Limata ldi has been amazing!! Best thing we did was buy this machine”
Richard Brady
GM
Circuitlabs
“Since 2019, we have been running the Limata X1000 LDI system (including LUVIR for solder mask imaging) in daily production as an addition to our current process with film. The machine was capable of properly exposing Taiyo PSR-4000 BN (DI) solder mask types on normal to high-copper boards using a new and unique direct imaging process. The machine operating interface is very user friendly which allowed for a quick technical training curve. The pre-registration processing reduced several seconds of production time at every print. Limata support and service staff is incomparable. They supported our team every step of the way at basically any time of the day or night, with literally, an immediate response time, customizing the software interface to best fit our Operations and needs.
We have exposed more than 8,000 prints since end of October, on various solder mask colors and some resist film panels. Limata, has proven to be very capable and innovative. They are a strong contender in the industry.
We have very much enjoyed this project, and working with the team!
Thank you Limata for the continued support and being a part of our growth.”
Bill Sezate
Vice President, GM
Summit Interconnect
As a replacement to our current contact exposure process with film, the LIMATA X2000 system including LUVIR-Technology was capable of properly exposing non-LDI solder mask types using a direct imaging process. The machine offers cutting edge software with a very intuitive operating interface which allowed for quick technician training curve. The dual drawer system combined with pre-registration processing reduced several seconds of production time at every machine cycle. Limata support and service staff is world class. They added software patches to keep production running at shortest possible response times, customized the software interface to best fit our in-house Operations system, and even wrote a step-by-step machine processing manual. As a result of the project, we have exposed more than 16,000 times on various product types and solder mask brands/colors. Limata, in a very short timeframe as a company, has definitely shown they are truly innovative and will be challenging the industry of direct imaging for the top spot.
Kevin Beattie
Process Engineer
TTM Technologies
Forest Grove Division